
Image not available

Medical & life sciences
Pharmaceutical Grade Gelatin Factory in China | Leading Bulk Suppliers
Leading pharmaceutical grade gelatin factory in China. Professional suppliers providing consistent quality, high transparency, and stable bulk supply for empty soft and hard capsules.
SupplierShijiazhuang Jinda Gelatin Co., Ltd.www.jindagelatin.com
Source categories
About this product
Product information from the supplier.
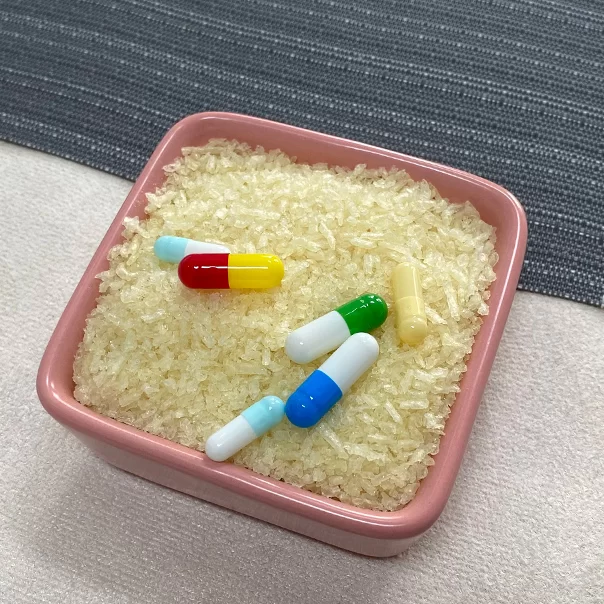
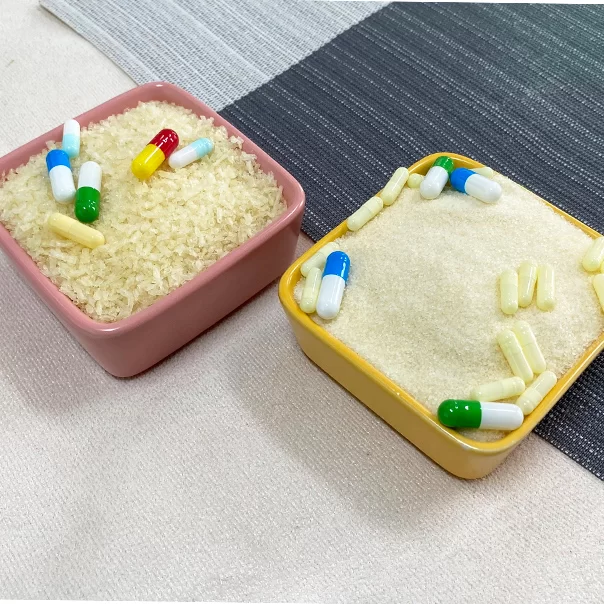
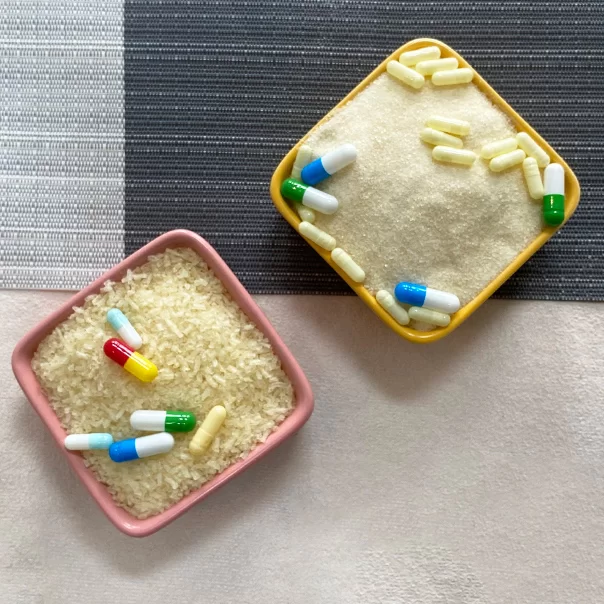
Jinda Pharmaceutical Grade Gelatin is a premium, high-purity protein derived from carefully selected bovine hides, specifically engineered to meet the stringent requirements of the pharmaceutical industry. This Halal-certified gelatin provides exceptional gelling, stabilizing, and thickening properties, ensuring the structural integrity and stability of medical delivery systems.
Designed for versatility and reliability, our pharmaceutical gelatin is the ideal choice for the production of hard and soft capsules, tablet binding, and microencapsulation. By combining advanced extraction technology with a stable raw material supply chain, we deliver consistent batch-to-batch quality that helps manufacturers optimize their production efficiency and product efficacy.
Detailed Parameters
| Manufacturer | Shijiazhuang Jinda Gelatin Co.,Ltd | Bloom Strength (6.67%) | 50-300 (As Required) |
|---|---|---|---|
| Viscosity (60℃) | 3.5-5 Mpa.s (As Required) | Mesh Size | 4-40 mesh |
| Transparency (mm) | 500 | Transmittance (450 nm) | ≥ 80% |
| Transmittance (620 nm) | ≥ 90% | Ash Content (w/%) | ≤ 2.0% |
| Moisture Content (w/%) | ≤ 14.0% | Shelf Life | 24 months |
Key Advantages
Stable Quality
Strict quality control ensures consistent performance and high purity for critical pharmaceutical applications.
Reliable Supply
Massive production capacity of 40mts per day guarantees a steady bulk supply for large-scale operations.
Wide Bloom Range
Flexible specifications from 50 to 300 bloom to suit diverse gelling and viscosity needs.
High Transparency
Exceptional clarity and transmittance for professional, high-quality capsule appearance.
Global Trust
An experienced global supplier trusted by pharmaceutical companies for purity and compliance.
Halal Certified
Sourced from selected bovine hides meeting strict Halal standards for global market accessibility.
Product Gallery
Management Platforms
Raw Material Sourcing
Selection of premium bovine hides to ensure the highest protein purity.
Advanced Processing
State-of-the-art equipment for precise Bloom and viscosity control.
QC Inspection
Rigorous testing for transmittance and ash content in every batch.
Halal Compliance
Strict adherence to bovine sourcing protocols for Halal certification.
Secure Packaging
25kg kraft paper bags with PE inner lining for moisture protection.
Logistics Efficiency
Fast delivery turnaround within 1-10 days for bulk pharmaceutical orders.
Investment Return Comparison
| Evaluation Metric | Standard Gelatin | Jinda Pharma Gelatin |
|---|---|---|
| Batch Consistency | Variable | High Stability |
| Supply Reliability | Moderate | 40mts/Day Capacity |
| Visual Clarity | Standard | Ultra-High Transparency |
| Production Waste | Higher (due to instability) | Minimized (consistent Bloom) |
| Market Compliance | Basic | Full Halal & Pharma Grade |
Frequently Asked Questions
Q: What are the primary applications of pharmaceutical grade gelatin?
It is primarily used for the production of hard and soft capsules, as a binder and coating agent for tablets, and in microencapsulation processes to protect active pharmaceutical ingredients.
Q: Can you provide custom Bloom strengths for specific needs?
Yes, we offer a wide range of Bloom strengths from 50 to 300, allowing us to customize the gelling strength and viscosity according to your specific product requirements.
Q: Is your bovine gelatin certified Halal?
Yes, our pharmaceutical grade gelatin is derived from selected bovine hides and processed in compliance with Halal standards to serve global pharmaceutical markets.
Q: What is the typical lead time for bulk orders?
We maintain a high production capacity of 40mts per day, enabling us to deliver bulk orders within 1 to 10 days depending on the order volume and destination.
Q: How is the product packaged to ensure quality during transit?
Our standard packaging consists of 25 kg kraft paper bags with a PE inner liner to prevent moisture contamination and maintain stability during shipping.
Q: Do you provide a Certificate of Analysis (COA) for each batch?
Yes, we provide comprehensive specifications and COA for every batch to ensure full transparency and compliance with pharmaceutical quality standards.
Ready to optimize your capsule production with high-purity gelatin?
Contact UsMore from this supplier
Shijiazhuang Jinda Gelatin Co., Ltd.


