
Image not available

Medical & life sciences
Medical PSA Oxygen Concentrator Factory Reliable China Suppliers of Hospital Oxygen Systems
Looking for reliable China suppliers? Our medical PSA oxygen concentrator factory provides high-purity on-site oxygen solutions for hospitals, reducing costs and ensuring an uninterrupted supply of medical-grade oxygen through advanced PSA technology.
SupplierHebei Lixin Medical Engineering Co., Ltd.www.storeoxygen.com
Source categories
About this product
Product information from the supplier.
Our New Medical PSA Oxygen Concentrator Equipment is a state-of-the-art solution engineered to meet the rigorous oxygen supply demands of modern healthcare facilities. Utilizing advanced Pressure Swing Adsorption (PSA) technology, this system efficiently extracts high-purity medical oxygen from ambient air, ensuring a steady, reliable flow that complies with stringent international healthcare standards for patient safety and therapeutic efficacy.
Designed for maximum reliability and operational simplicity, the system integrates high-performance compressors, precision molecular sieve beds, and intelligent control systems. Its modular architecture allows for seamless scalability, making it an ideal choice for a wide spectrum of medical environments, from specialized outpatient clinics to large-scale comprehensive medical centers, effectively reducing dependency on costly oxygen cylinders and liquid oxygen logistics.
Detailed Parameters
| Oxygen Purity | 90-96% | Production Capacity | 1-60 cubic meters |
|---|---|---|---|
| Operational Principle | Molecular Sieve PSA | Voltage Requirement | 380V |
| Noise Level | 70 (dB) | Certification | ISO9001 |
| Warranty Period | 1 Year | Energy Status | Energy Saving |
| Transport Package | Wooden Box | Origin | Hebei Hengshui |
Key Advantages
Uninterrupted Supply
On-site generation eliminates risks associated with cylinder replacements and delivery delays during emergencies.
Operational Efficiency
Automated PSA cycles and intelligent monitoring reduce the manual workload for medical staffing.
High Precision
Delivers precise oxygen flow rates and high purity levels tailored to individual patient clinical needs.
Intelligent Control
Equipped with real-time purity monitoring, automatic alarms, and secure automatic shutdown features.
Modular Scalability
Flexible design allows the system to grow alongside the facility's patient volume and demand.
Cost Reduction
Significantly lowers logistical costs by removing the need for external liquid oxygen transportation.
Product Gallery
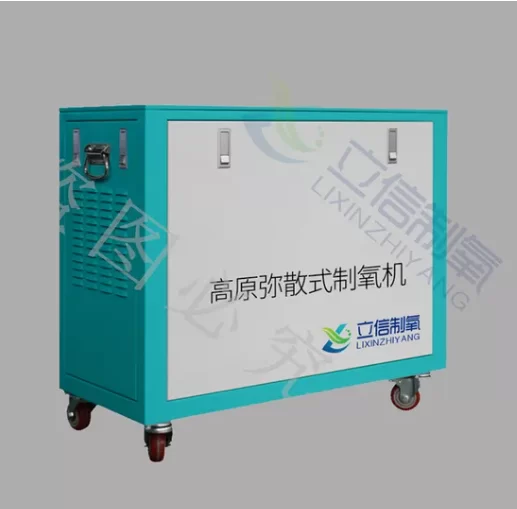
Management Platforms
Purity Monitoring
Real-time digital tracking of oxygen concentration to ensure therapeutic grade purity.
Automated Control
Intelligent PSA switching and pressure regulation for seamless continuous operation.
Safety Alarms
Instant notifications for low purity, pressure drops, or system malfunctions.
Filtration Management
Scheduled reminders for air intake and particulate filter cleaning and replacement.
Energy Tracking
Optimized power consumption monitoring to reduce overall facility operational costs.
Remote Diagnostics
Digital interfaces for quick troubleshooting and system performance evaluation.
Investment Return Comparison
| Comparison Factor | Traditional Cylinder Supply | Medical PSA System |
|---|---|---|
| Supply Reliability | Dependent on Logistics | On-site Independent |
| Operational Cost | High Recurring Cost | Low Energy-based Cost |
| Storage Space | Large Storage Required | Compact Installation |
| Labor Requirement | High (Manual Handling) | Low (Automated) |
| Safety Risk | High Pressure Gas Risk | Controlled Atmospheric Extraction |
Frequently Asked Questions
Q: What is the typical purity level of the PSA oxygen concentrator?
Our systems are designed to provide medical-grade oxygen with a purity range of 90% to 96%, meeting international healthcare standards for patient respiratory support.
Q: How does a PSA oxygen generator reduce hospital costs?
By producing oxygen on-site from ambient air, hospitals eliminate the need for frequent liquid oxygen deliveries and cylinder rentals, significantly cutting logistics and procurement costs.
Q: What maintenance is required for these medical concentrators?
Routine maintenance includes regular inspection and replacement of air intake filters, monitoring oxygen purity via sensors, and periodic mechanical checks of the compressor and valves.
Q: Can this system be scaled for larger medical centers?
Yes, the modular design allows for the addition of more molecular sieve beds and compressors to increase the production capacity from 1 up to 60 cubic meters.
Q: Is the equipment safe for ICU and surgical environments?
Absolutely. The system includes real-time monitoring, automated alarms, and automatic shutdown features to ensure the highest safety standards for critical care patients.
Q: What are the power requirements for the PSA system?
The standard industrial model operates on a 380V voltage system to ensure powerful and stable compression for continuous oxygen generation.
Ready to Modernize Your Hospital Oxygen Supply?
Contact UsMore from this supplier
Hebei Lixin Medical Engineering Co., Ltd.


