Image not available
Industrial manufacturing
HighEfficiency LNG Gasification Equipment Suppliers from China Factory
Looking for reliable LNG gasification equipment? As leading China suppliers and a professional factory, we provide integrated LNG satellite stations for receiving, storage, and distribution, offering an eco-friendly transition to cleaner energy for cities and industrial zones.
SupplierHEBEI OUYINUO GAS EQUIPMENT CO.,LTD.www.gasouyinuo.com
Source categories
About this product
Product information from the supplier.
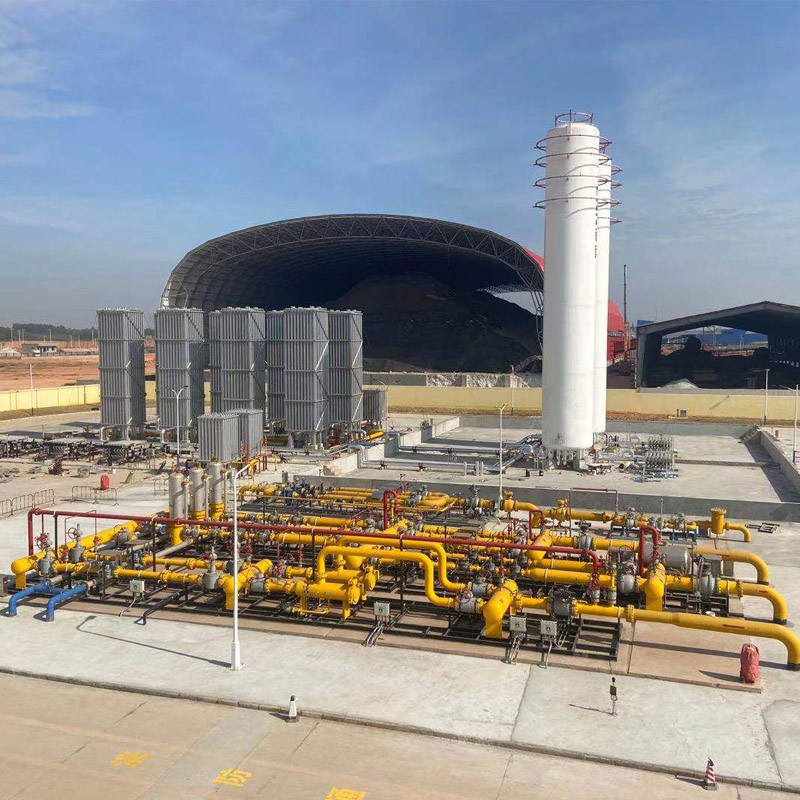
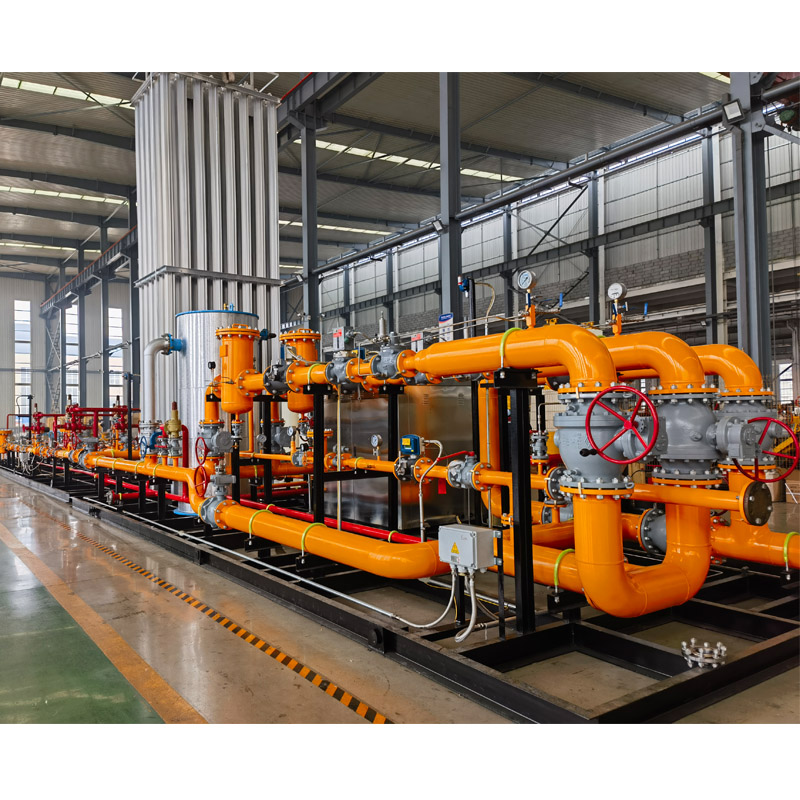
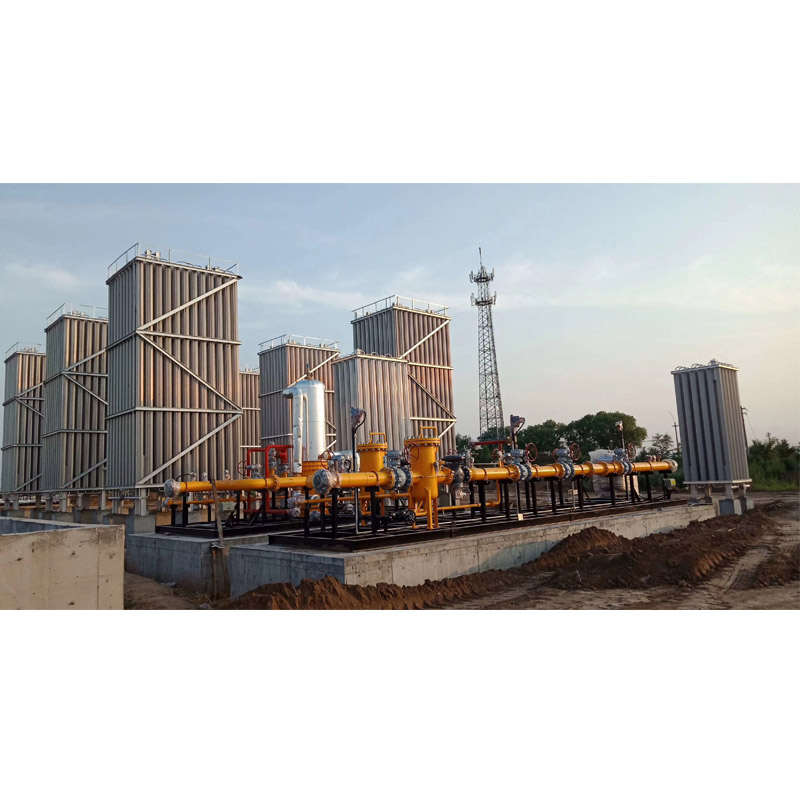
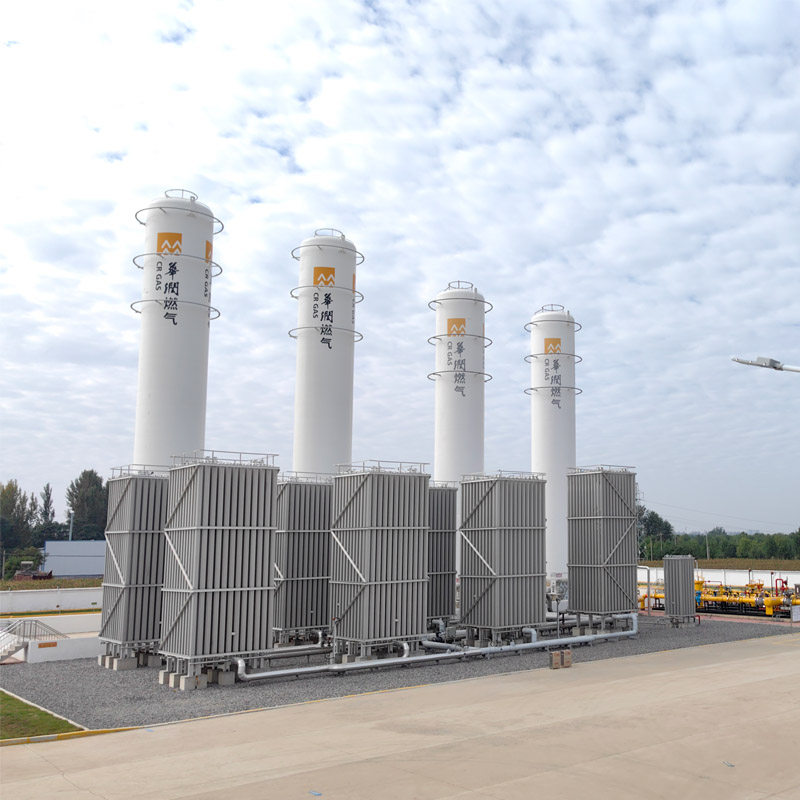
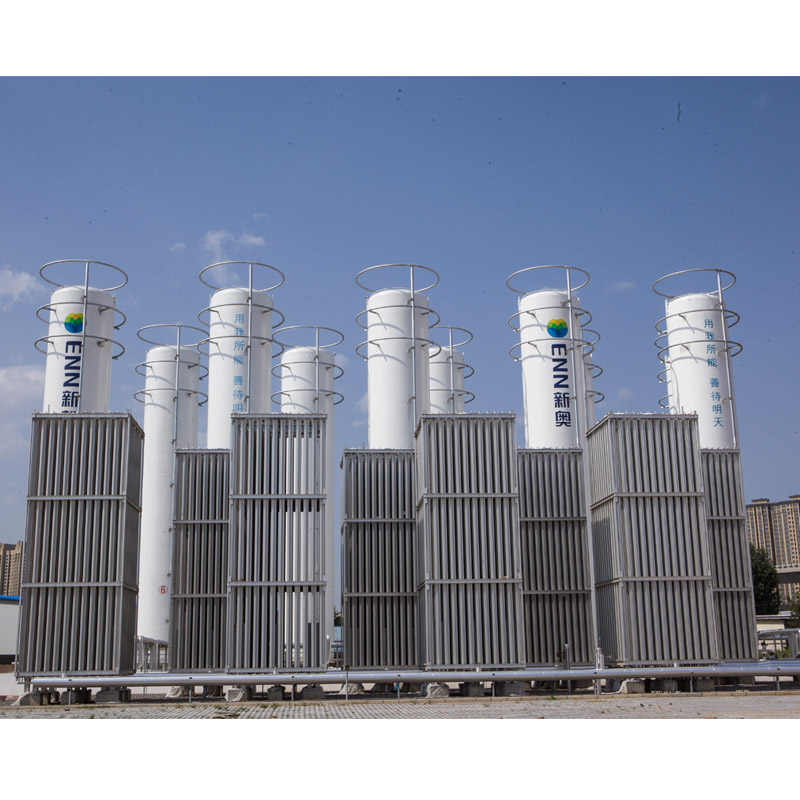
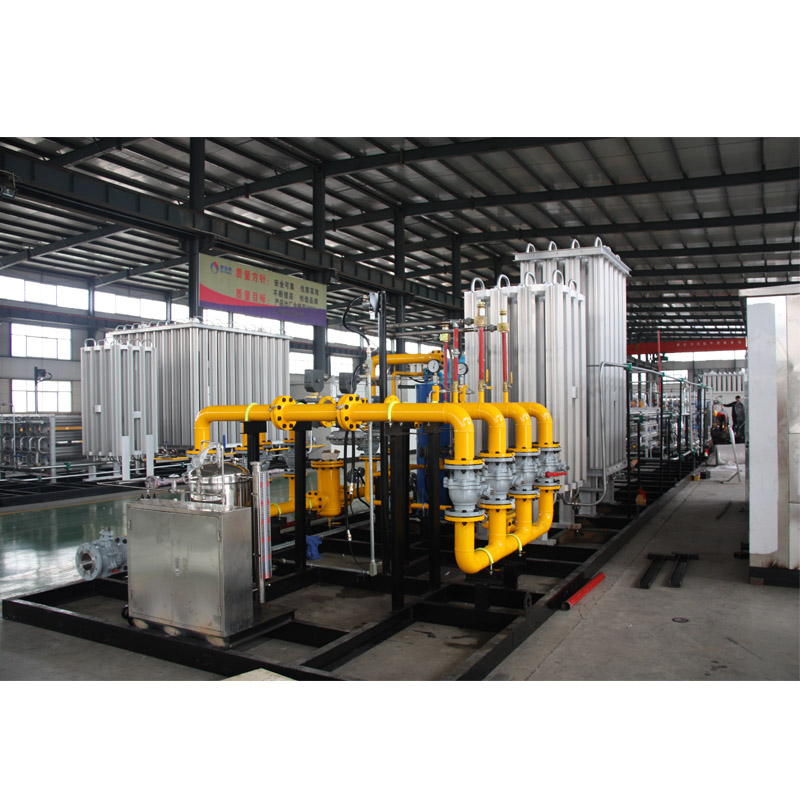
Our advanced LNG Gasification Equipment provides a comprehensive solution for cities and industrial zones transitioning to cleaner energy. As a high-efficiency LNG satellite station, this system integrates receiving, cryogenic storage, and distribution functions, acting as a critical intermediate regulation hub that seamlessly transfers Liquefied Natural Gas from manufacturers to end-users. Designed for rapid deployment, it effectively meets urgent gas market demands in energy-deficient regions before the arrival of permanent pipeline infrastructure.
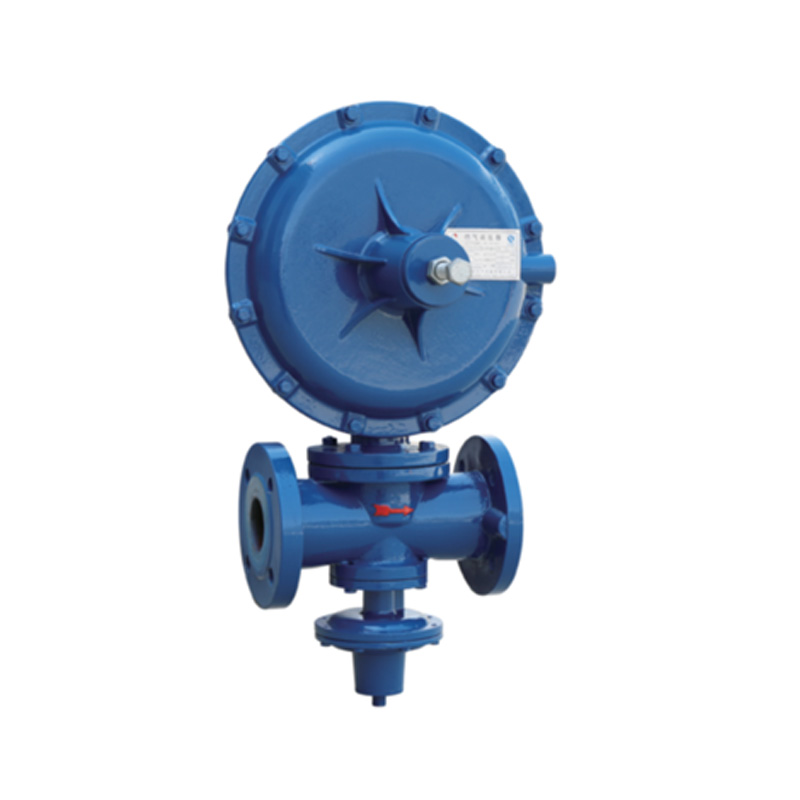
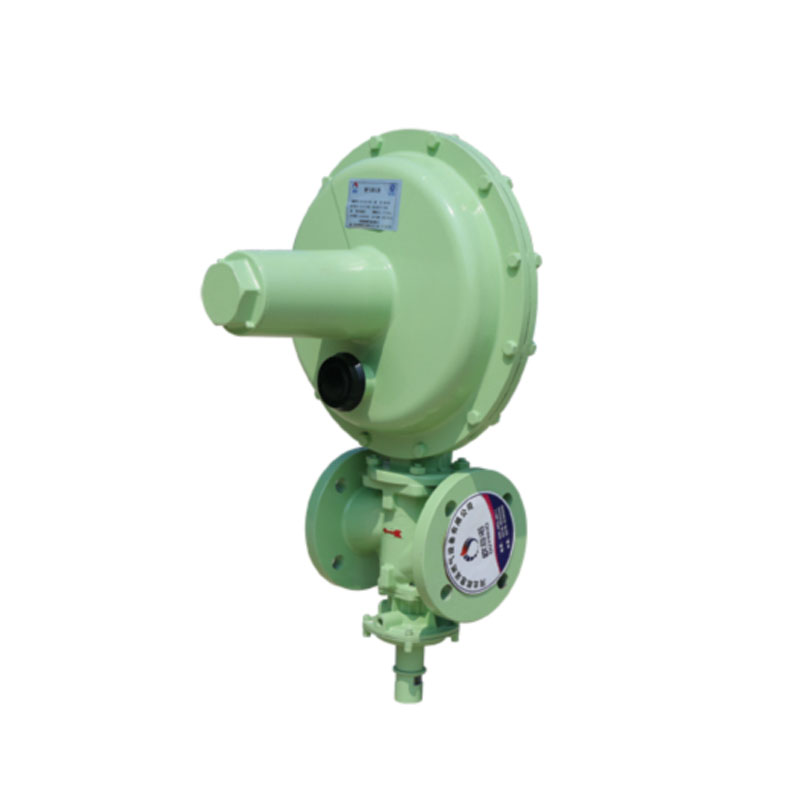
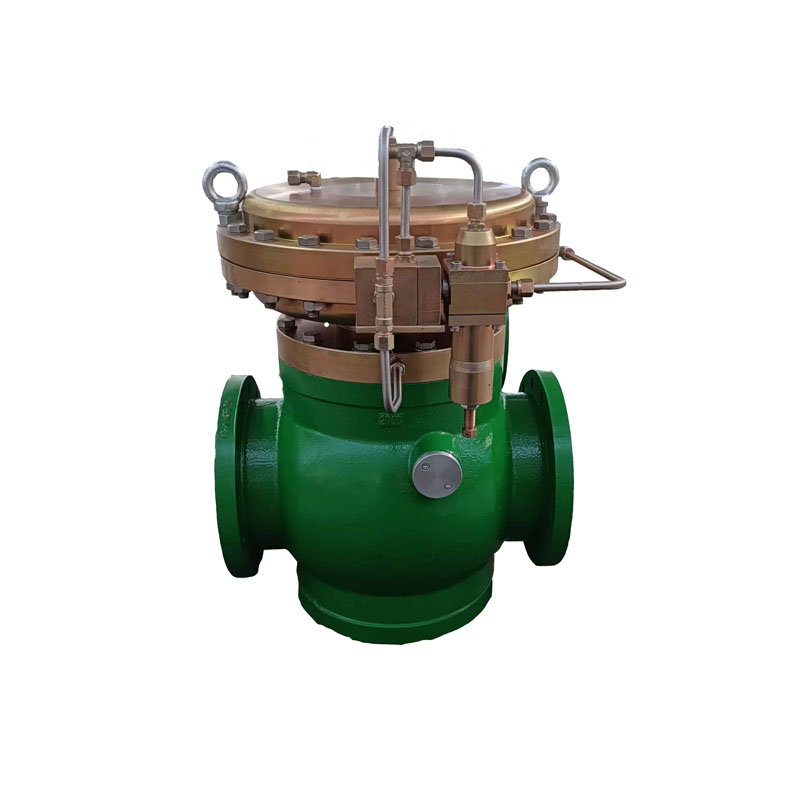
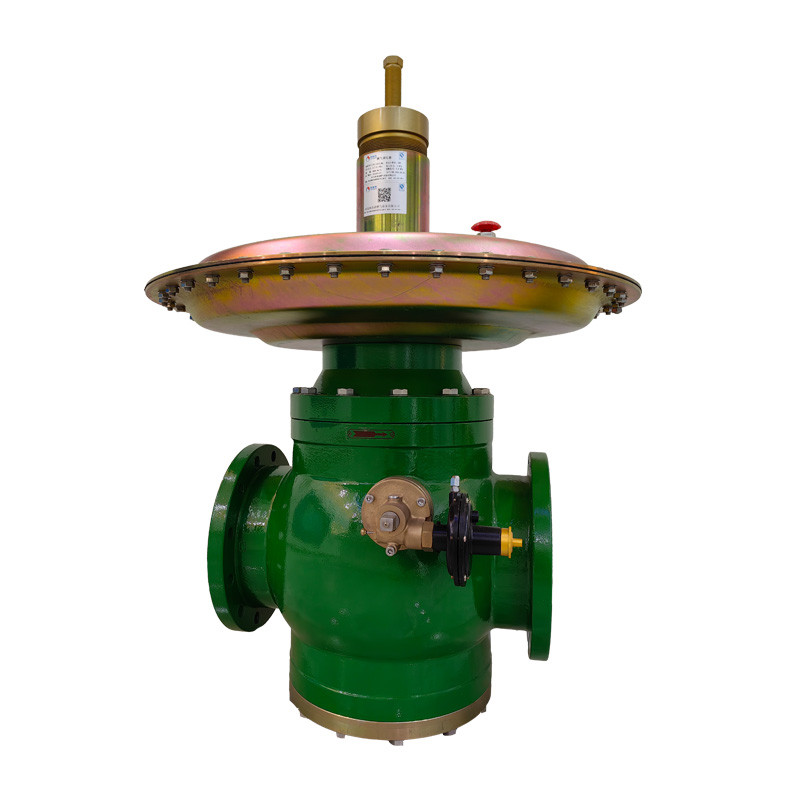
The system is engineered for maximum reliability and automation, integrating low-temperature storage tanks, air-heated vaporizers, precision pressure reducing valves, chemical dosing systems, and advanced metering. By leveraging a sophisticated technological process—from unloading pressurization to odorization—the equipment ensures a steady, safe flow of natural gas into municipal networks, maintaining optimal temperature and pressure regardless of ambient conditions.
Detailed Parameters
| Design Pressure | 1.6 MPa | Strength Test Pressure | 2.4 MPa |
|---|---|---|---|
| Airtight Test Pressure | 1.92 MPa | Operating Pressure | 0.02 - 0.8 MPa |
| Vaporization Capacity | 20 - 10,000 Nm³/h | Design Temperature | -196℃ to +50℃ |
| Outlet Pressure | ≤ 0.4 MPa | Safety Valve Opening | 0.84 MPa |
| Flowmeter Accuracy | Level 1.0 - 1.5 | Recuperative Voltage | 380 V |
Key Advantages
Zero Emission
Operates with no energy consumption and zero contamination, ensuring an eco-friendly gasification process.
Low OpEx
Optimized design reduces long-term operating costs and minimizes maintenance requirements.
Optimal Efficiency
Engineered for low pressure drop and high vaporization quantity to meet strict industrial requirements.
Thermal Stability
Aluminum "bridge" connections eliminate stress caused by heat expansion and cold contraction.
Standardized Build
Manufactured according to JB/T2549-94 and Q/OYN01-2017 technical specifications for air separation plants.
Safety Guaranteed
Includes complete safety protection functions and auxiliary heaters to ensure stable outlet temperatures.
Product Gallery
Management Platforms
Storage Monitoring
Real-time tracking of LNG levels in low-temperature storage tanks to prevent supply shortages.
Pressure Regulation
Automated control of pressure reducing valves to maintain consistent pipeline network flow.
Safety Alerts
Instant notification system for safety valve activations or pressure deviations.
Thermal Control
Intelligent activation of water bath heaters when ambient temperatures drop below 5℃.
Metering Analytics
High-precision flowmeter data integration for accurate consumption and distribution auditing.
Odorization Mgmt
Controlled dosing systems to ensure natural gas safety standards through precise odorization.
Investment Return Comparison
| Metric | Standard Gasification | Our Integrated Solution |
|---|---|---|
| Construction Period | Long / Complex | Short / Rapid Deployment |
| Energy Consumption | High (External Heat) | Zero (Air-Heated) |
| Operating Costs | Moderate to High | Very Low |
| Automation Level | Manual/Semi-Auto | Fully Automated |
| Environmental Impact | Potential Emissions | Eco-Friendly / No Pollution |
Frequently Asked Questions
Q: What is the main function of an LNG gasification station?
It serves as a satellite station that receives, stores, and converts liquid LNG back into gaseous natural gas for distribution to municipal pipelines or industrial users.
Q: How does the equipment handle extremely low outdoor temperatures?
When ambient temperatures are low and the outlet temperature falls below 5℃, a configured water bath auxiliary heater is used to ensure the gas remains at a safe temperature.
Q: What are the safety standards used in manufacturing?
All components are manufactured according to JB/T2549-94 Technical Specifications for Aluminum-made Air Separation Plants and Q/OYN01-2017 Enterprise Standards.
Q: What is the range of vaporization capacity available?
Our systems are scalable, offering vaporization capacities ranging from 20 Nm³/h up to 10,000 Nm³/h to suit various demand levels.
Q: Does the gasification process consume external energy?
The primary air-heated vaporizer is designed for zero energy consumption, significantly reducing operating costs and environmental impact.
Q: How is the LNG delivered from the tanker to the storage tank?
An LNG unloading pressurizer is used to increase the pressure in the tanker, allowing the liquid LNG to be delivered efficiently into the low-temperature storage tank.
Ready to Optimize Your Gas Supply Infrastructure?
Contact UsMore from this supplier
HEBEI OUYINUO GAS EQUIPMENT CO.,LTD.