Image not available
Industrial manufacturing
AWS ENiCl Cast Iron Welding Rods Factory and Suppliers in China
Buy high-quality AWS ENi-Cl THZ308 pure nickel cast iron welding rods from a leading China factory. Our suppliers provide electrodes with strong reduction graphite coating, requiring no preheating and offering excellent crack resistance for industrial repairs.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
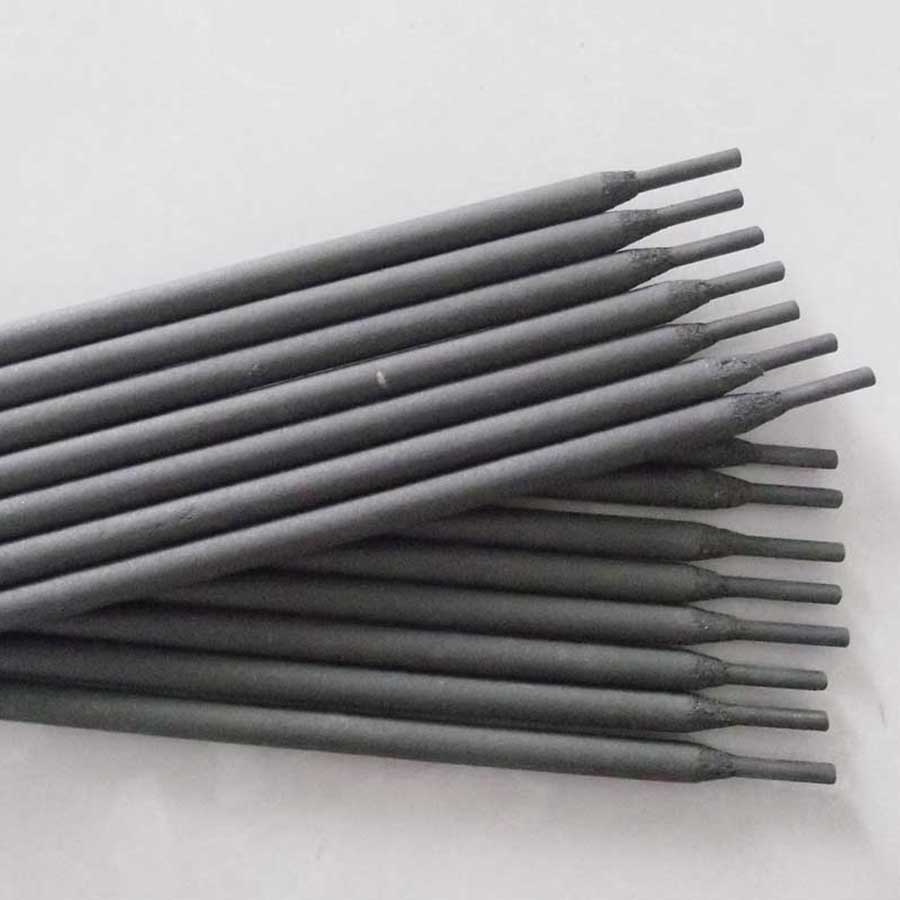
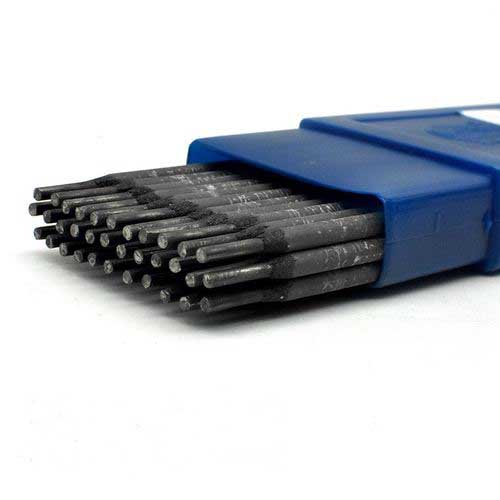
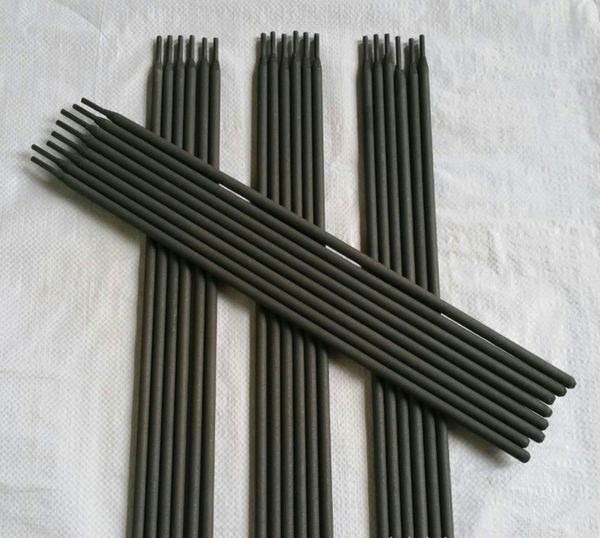
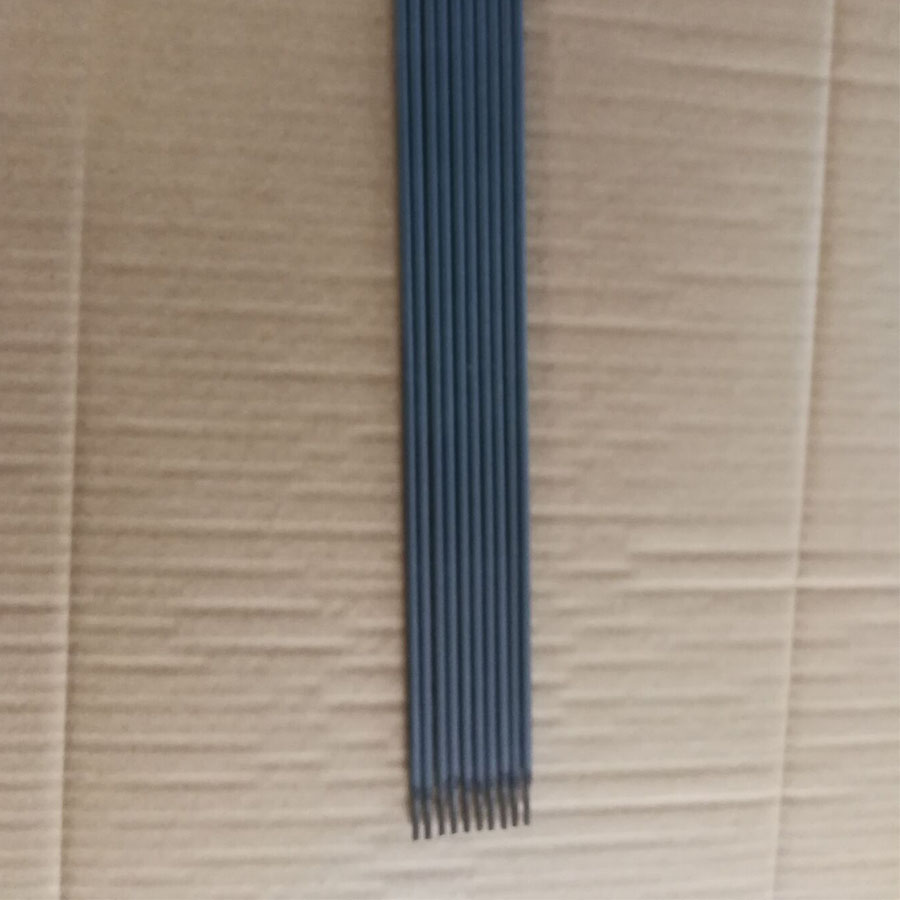
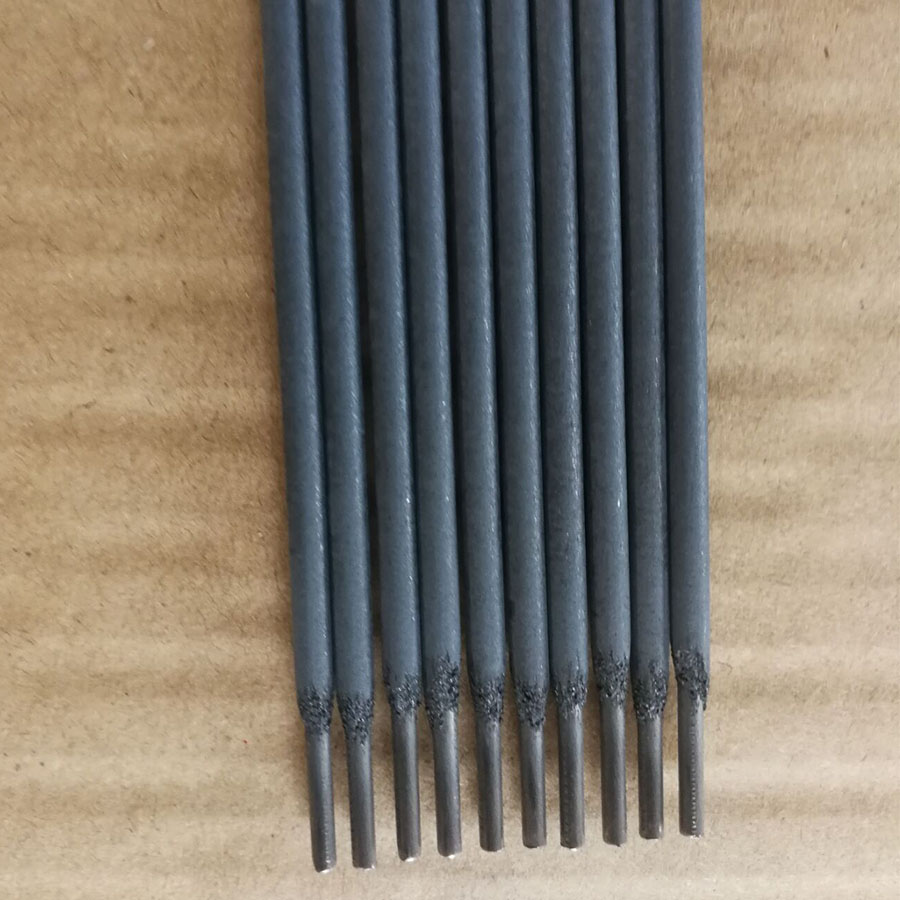
The Cast Iron Welding Rod Electrode AWS ENi-Cl (THZ308) is a professional-grade welding solution featuring a pure nickel core and a strong reduction graphite-type coating. Specifically engineered for the demanding requirements of cast iron repair, this electrode is compatible with both AC and DC power sources, ensuring versatility across various industrial environments and equipment setups.
Designed to eliminate the need for preheating, the ENi-Cl electrode provides exceptional crack resistance and superior processability. It is the ideal choice for repairing critical components such as engine shells, machine bases, and casting teeth, effectively solving common industrial issues including wheel breakage, wear, and punching holes through high-performance metallurgical bonding.
Detailed Parameters
| Classification | AWS ENi-Cl / THZ308 | Core Material | Pure Nickel |
|---|---|---|---|
| Coating Type | Strong Reduction Graphite | Current Type | AC / DC Dual Purpose |
| Preheating | Not Required | Welding Positions | PA, PB |
| Application | Cold Welding Cast Iron | Main Benefit | High Crack Resistance |
| Baking Temp | 150±10℃ (1 Hour) | Base Material | Fe-C-Si Alloys |
Key Advantages
Crack Resistance
Superior metallurgical properties prevent weld cracking and ensure structural integrity in brittle cast iron.
No Preheating
Saves significant time and energy by allowing high-quality cold welding without the need for heat treatment.
Easy Operation
Optimized arc stability makes it easy to operate for both experienced welders and maintenance technicians.
Versatile Application
Perfect for engine covers, machine bases, and casting teeth across multiple industrial sectors.
Precise Processability
Excellent post-weld machinability allows for easy grinding and finishing of the repaired surface.
Dual Compatibility
Full support for both AC and DC currents, offering maximum flexibility for different welding machines.
Product Gallery
Management Platforms
Inventory Control
Real-time tracking of welding rod stock to ensure uninterrupted production lines.
Quality Assurance
Strict adherence to AWS standards for every batch of nickel-core electrodes produced.
Technical Support
Expert guidance on current settings and groove preparation for cast iron welding.
Order Tracking
Transparent logistics management from our factory to your industrial site.
Packaging Options
Customized moisture-proof packaging to maintain electrode coating integrity.
Process Optimization
Consultancy on transitioning from hot welding to efficient cold welding methods.
Investment Return Comparison
| Feature | Traditional Hot Welding | ENi-Cl Cold Welding |
|---|---|---|
| Energy Cost | High (Constant heating) | Low (No preheating) |
| Time Efficiency | Slow (Wait for cooling) | Fast (Immediate start) |
| Crack Risk | Medium/High | Very Low |
| Equipment Need | Industrial Furnaces | Standard Welding Machine |
| Labor Cost | High (Multi-stage process) | Reduced (Single stage) |
Frequently Asked Questions
Q: Why do I need to bake the ENi-Cl electrodes before use?
Baking electrodes at 150±10℃ for one hour removes moisture from the coating, preventing porosity and ensuring a stable arc during the welding process.
Q: How can I further prevent cracks in cast iron welding?
It is recommended to hammer the welding seam to eliminate residual stress and use the smallest possible current to reduce the width of the white band.
Q: What is the best groove preparation for cast iron repair?
The joint should be obliquely cut into a U-shaped groove. Additionally, stop-crack holes should be drilled at both ends of the crack to prevent expansion.
Q: Which welding positions are suitable for these electrodes?
These electrodes are designed for PA (flat) and PB (horizontal) welding positions, providing excellent bead control in these orientations.
Q: Can this electrode be used on all types of cast iron?
Yes, it is effective for Fe-C-Si based industrial cast irons, commonly found in engine shells, machine bases, and various casting parts.
Q: What is the recommended technique for filling the weld joint?
Use short and thin welding beads with a narrow lateral swing of the torch. Maintain a medium arc length and a slight incline in the welding direction.
Get Professional Technical Support for Your Welding Projects
Contact UsNeed a quick quotation for ENi-Cl? Chat with us on WhatsApp or email info@steeltoolschina.com.
Browse the cast iron welding rods collection, or see every welding electrode we manufacture.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.