Image not available
Industrial manufacturing
AWS E7018 Low Hydrogen Welding Rods Factory Suppliers in China
Looking for high-quality AWS E7018 basic coated iron powder low potassium hydrogen type electrodes? We are leading China factory suppliers providing X-ray quality welding rods with exceptional crack resistance.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
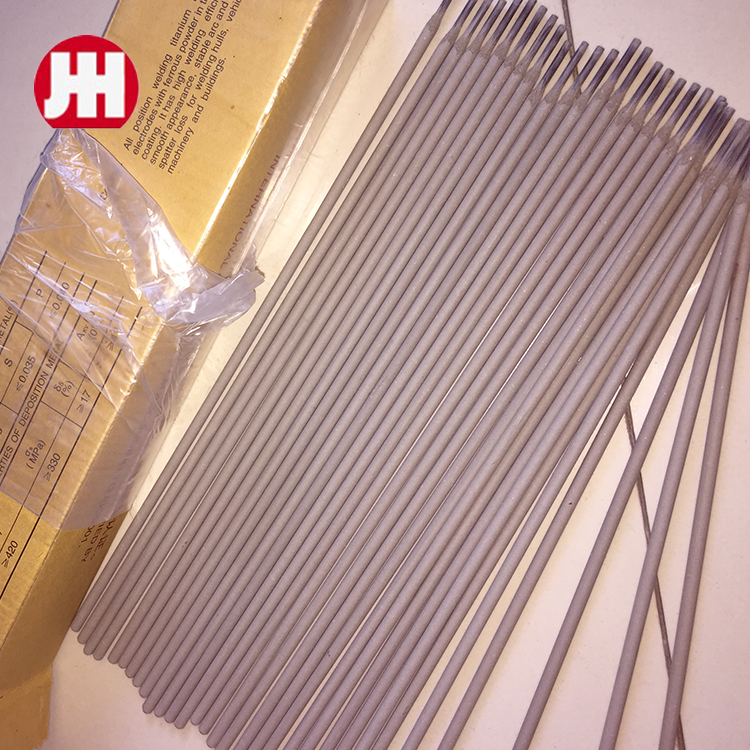
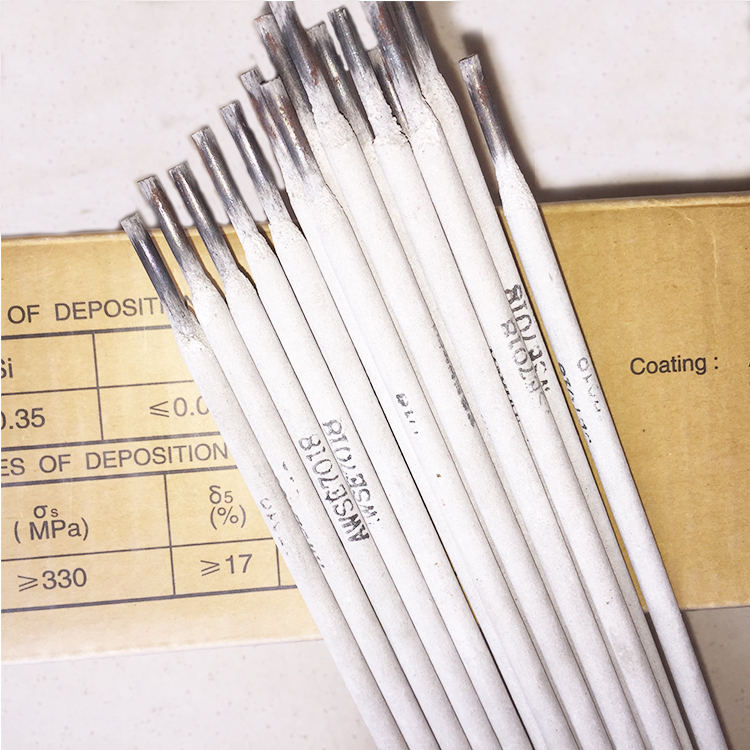
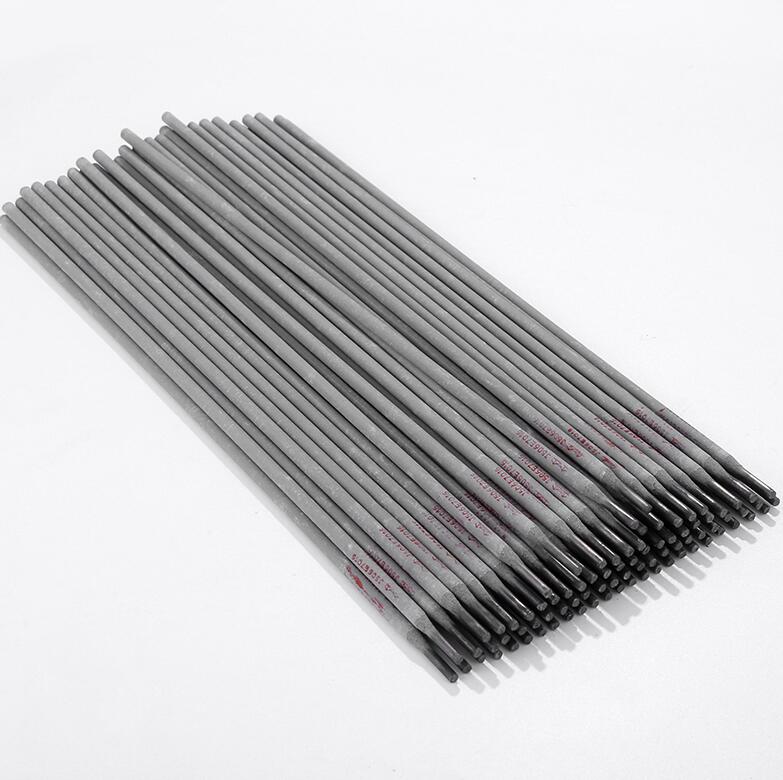
AWS E7018 is a premium, basic-coated iron powder, low-potassium hydrogen-type electrode designed for high-strength applications. Engineered for versatility, it supports both AC and DC currents and is fully capable of all-position welding, ensuring exceptional performance across diverse industrial environments.
This professional-grade electrode is renowned for its superior arc stiffness, minimal spatter, and efficient slag removal, resulting in a clean, aesthetic weld bead. With high deposition efficiency and excellent low-temperature toughness, E7018 provides the structural integrity and crack resistance required for the most demanding metal fabrication projects.
Detailed Parameters
| AWS Classification | E7018 | Coating Type | Basic Coated (Low Hydrogen) |
|---|---|---|---|
| Current Type | AC / DC | Welding Position | All Position (PA, PB, PC, PD, PE, PF) |
| Tensile Strength | 70 ksi (Minimum) | X-Ray Detection | Level I (Excellent) |
| Core Feature | Iron Powder Added | Slag Removal | Easy / Rapid |
| Re-baking Temp | 350-400°C | Re-baking Time | 1-2 Hours |
Key Advantages
Crack Resistance
Exceptional stable low-temperature toughness prevents cracking in critical structural welds.
High Efficiency
Iron powder in the coating significantly increases deposition rates and overall productivity.
Superior Finish
Produces fine, clean weld shapes with minimal spatter for a professional, polished appearance.
Stable Arc
Excellent arc stiffness prevents magnetic deflection, ensuring precise control during welding.
All-Position Use
Versatile application across all positions (PA-PF) makes it ideal for complex assemblies.
X-Ray Quality
Meets Level I X-ray flaw detection standards, ensuring maximum internal weld purity.
Product Gallery
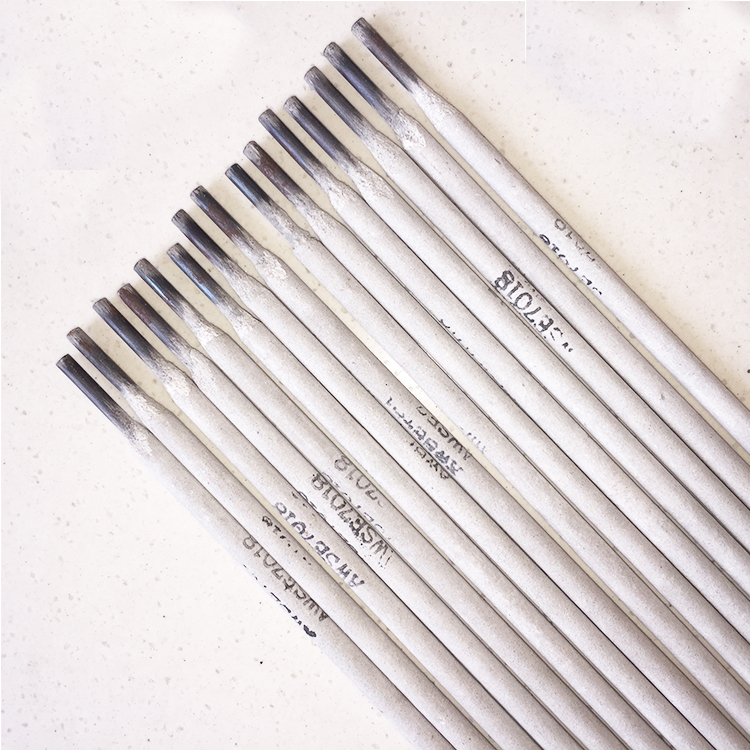
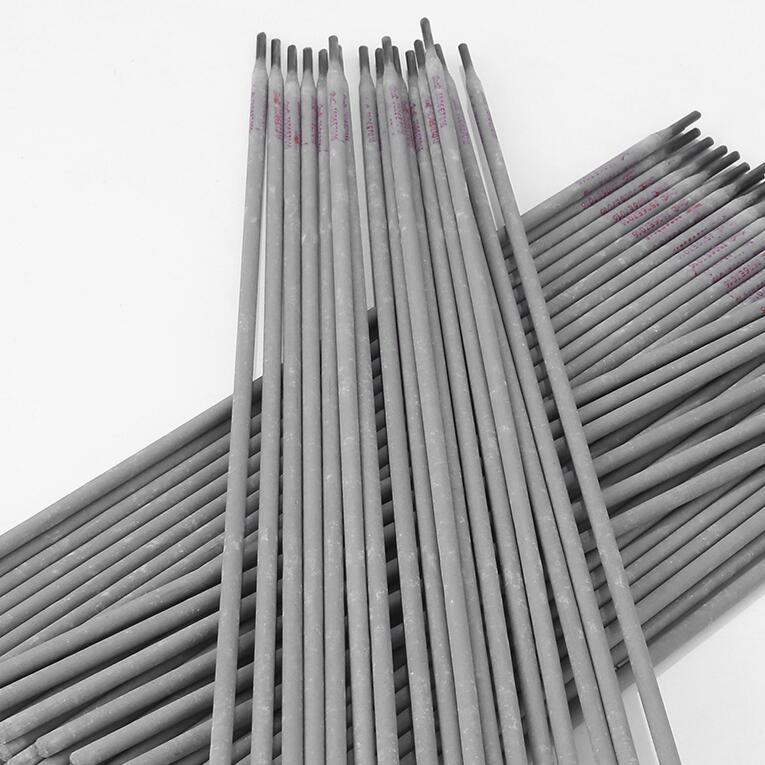
Management Platforms
Quality Control
Rigorous inspection of basic coating chemistry to ensure low hydrogen levels.
Production Precision
Advanced extrusion technology for consistent electrode diameter and coating thickness.
Storage Protocol
Strict climate-controlled warehousing to prevent moisture absorption.
Baking Standards
Standardized re-baking procedures at 350-400°C to restore coating performance.
Supply Chain
Optimized logistics for rapid delivery of high-volume industrial orders.
Technical Support
Expert guidance on adjusting parameters for specific material replacements.
Investment Return Comparison
| Feature Comparison | Standard Electrodes | AWS E7018 Premium |
|---|---|---|
| Deposition Rate | Standard | High (Iron Powder Enhanced) |
| Weld Aesthetics | Average Spatter | Clean, Fine Bead |
| Structural Integrity | Moderate Toughness | Excellent Low-Temp Toughness |
| Inspection Success | Variable | X-Ray Level I Certified |
| Operational Cost | Higher Waste | Lower Waste / Higher Efficiency |
Frequently Asked Questions
Q: Why is it necessary to store E7018 welding rods in a drying oven?
E7018 electrodes are low-hydrogen types and are highly prone to absorbing moisture from the air. To maintain their chemical properties and prevent hydrogen-induced cracking, they must be stored in a specialized drying oven.
Q: How should I re-bake E7018 electrodes if they have been exposed to air?
Electrodes exposed to atmospheric moisture should be re-baked at temperatures between 350-400°C for 1 to 2 hours to restore the performance of the coating.
Q: Can E7018 be used for mild steel without baking?
While mild steel can be welded with unbaked E7018 electrodes, it is not recommended for critical work as the weld strength may not reach the required high specifications.
Q: What does the "70" and "18" in E7018 signify?
The "70" refers to the minimum tensile strength of the weld metal (70 ksi), while "18" indicates the welding position (all-position), the coating type (low hydrogen), and the compatible welding currents (AC or DC).
Q: How does the iron powder coating benefit the welding process?
The addition of iron powder increases the deposition efficiency, allowing more metal to be deposited per hour, while also stabilizing the arc and reducing spatter.
Q: What precautions should be taken when replacing E7018 with other electrodes?
If you must replace E7018 with a different specification, you must adjust the welding process parameters (current, voltage, speed) according to the material's specific conditions to ensure quality is controllable.
Get a Factory Direct Quote for AWS E7018 Welding Rods
Contact UsNeed a quick quotation for E7018? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full E7018 low hydrogen electrodes range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.