Image not available
Industrial manufacturing
Premium E7018 Welding Electrodes Factory and Suppliers in China
Looking for high-strength E7018 welding electrodes? As leading China suppliers and factory, we provide iron powder type basic electrodes conforming to GB/T 5117 E5018, AWS A5.1 E7018, and ISO 2560-B-E4918 A for superior weld integrity.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
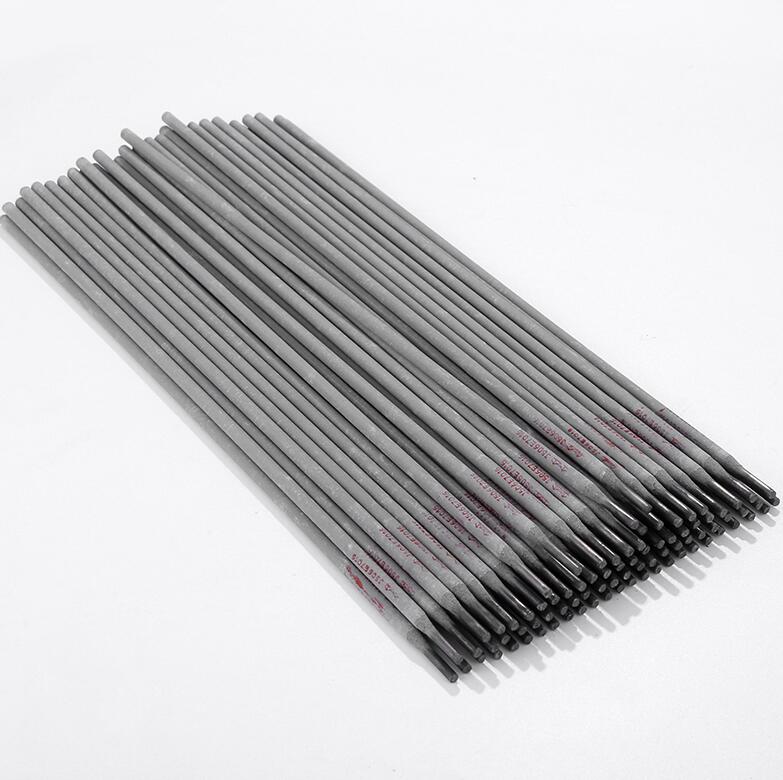
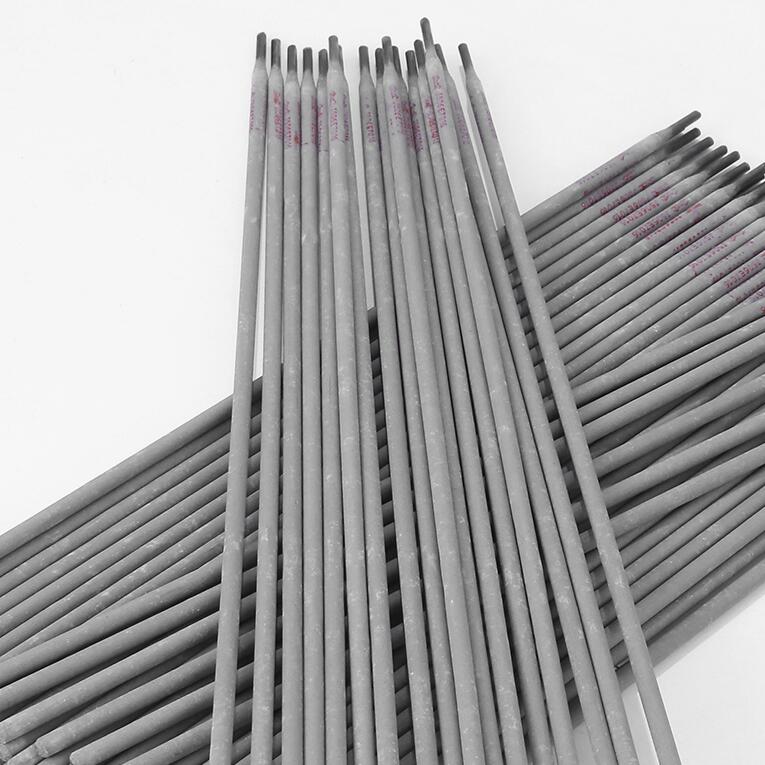
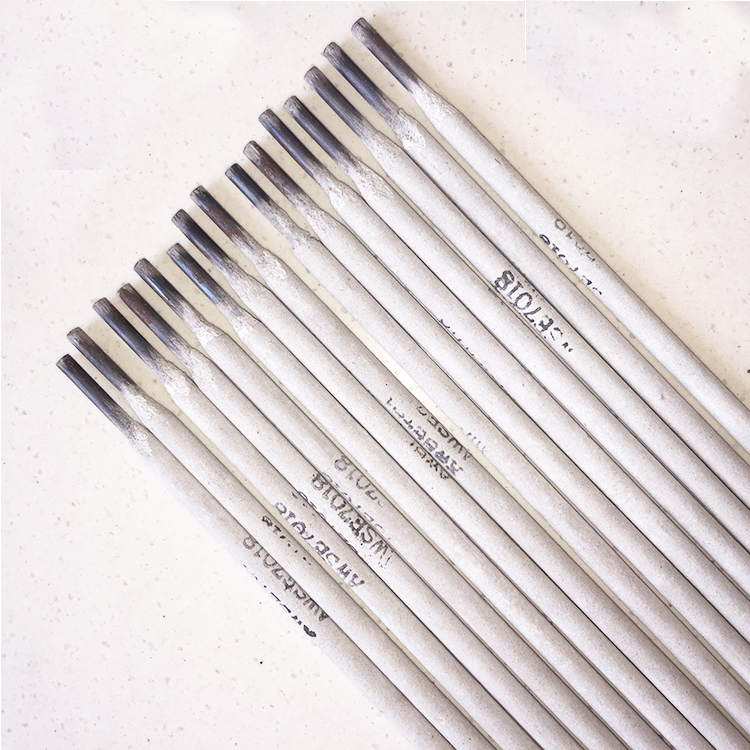
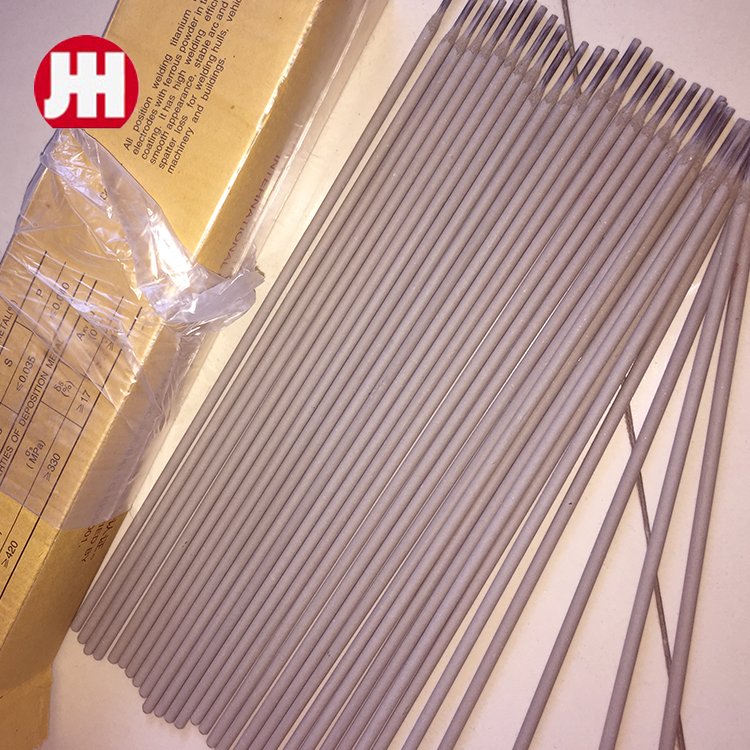
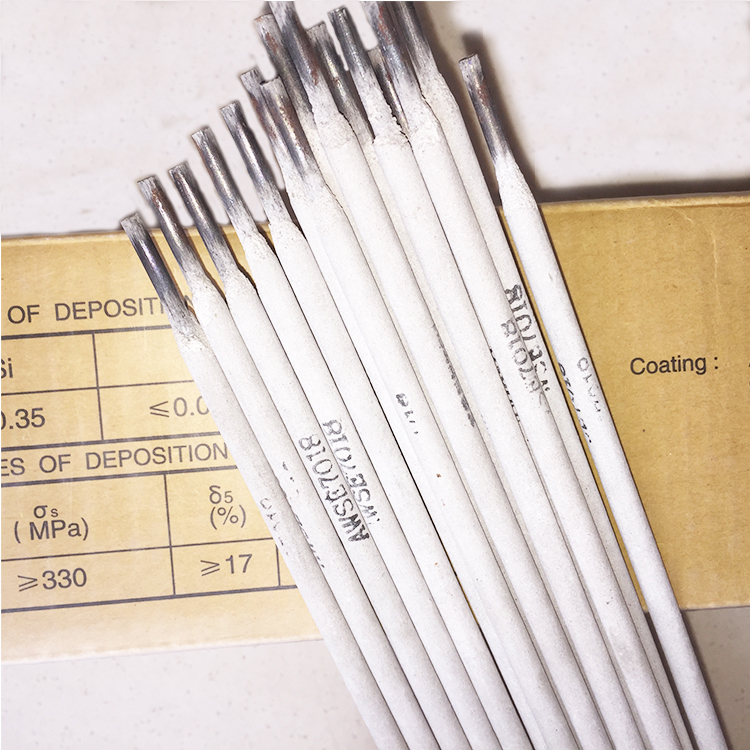
The E7018 welding electrode is a premium-grade, low-hydrogen potassium basic coated electrode enriched with iron powder. Specifically engineered for high-strength applications, it conforms to international standards including AWS A5.1 E7018, GB/T 5117 E5018, and ISO 2560-B-E4918. This professional-grade tool is designed to deliver exceptional mechanical performance and superior weld integrity across all positions, making it an indispensable choice for critical structural welding.
Designed for versatility, these electrodes are compatible with both AC and DC currents, ensuring stable arc stiffness and minimal spatter. The inclusion of iron powder in the coating significantly enhances deposition efficiency, while the low-hydrogen formulation prevents crack formation and ensures excellent low-temperature toughness. Whether you are working on high-strength carbon steel or low-alloy steels, the E7018 provides a clean, aesthetically pleasing weld bead with effortless slag removal.
Detailed Parameters
| AWS Classification | E7018 | ISO Standard | ISO 2560-B-E4918 A |
|---|---|---|---|
| GB/T Standard | GB/T 5117 E5018 | Coating Type | Low Hydrogen Potassium / Basic |
| Current Type | AC / DC | Welding Position | All Position (PA, PB, PC, PD, PE, PF) |
| X-ray Detection | Level I (Excellent) | Available Sizes | 3.2mm, 4.0mm |
| Key Feature | Iron Powder Enhanced | Primary Use | High-strength Carbon & Low-alloy Steel |
Key Advantages
Crack Resistance
Low-hydrogen formulation significantly reduces the risk of hydrogen-induced cracking, ensuring structural safety.
High Efficiency
Integrated iron powder increases the deposition rate, reducing overall welding time and labor costs.
Stable Arc
Excellent arc stiffness ensures a stable welding process with minimal spatter and magnetic deflection.
Clean Finish
Produces fine, clean weld beads with easy-to-remove slag for a professional aesthetic appearance.
Low-Temp Toughness
Maintains excellent plasticity and mechanical strength even in low-temperature environments.
All-Position Versatility
Optimized for PA, PB, PC, PD, PE, and PF positions, offering total flexibility on-site.
Product Gallery
Management Platforms
Moisture Control
Strict monitoring of flux coating dryness to prevent hydrogen absorption from the atmosphere.
Baking Protocol
Standardized re-baking at 350-400°C for 1-2 hours to restore optimal coating performance.
Exposure Limits
Rigid 4-hour air exposure limit for standard and 9-hour limit for H4R suffix electrodes.
Quality Certification
Full compliance with AWS and ISO standards ensuring consistency across every batch.
Storage Solutions
Utilization of professional welding rod drying ovens to maintain low-hydrogen integrity.
Surface Preparation
Guided joint design and cleaning processes to minimize weld discontinuities.
Investment Return Comparison
| Performance Metric | Standard Electrodes | E7018 Low-Hydrogen |
|---|---|---|
| Deposition Rate | Moderate | High (Iron Powder Enhanced) |
| Weld Integrity | Basic | Superior (X-ray Level I) |
| Crack Risk | Higher in High-Strength Steel | Extremely Low |
| Post-Weld Cleaning | Time Consuming | Efficient (Easy Slag Removal) |
| Application Range | Limited Positions | All-Position Versatility |
Frequently Asked Questions
Q: Why is baking necessary for E7018 welding rods?
E7018 is a low-hydrogen electrode. Its coating absorbs moisture from the air quickly. Baking at 350-400°C removes this moisture, preventing hydrogen from entering the weld, which avoids porosity and cold cracking.
Q: What does the H4R suffix mean on some E7018 electrodes?
The H4R suffix indicates a more moisture-resistant coating, allowing the electrode to maintain its performance in open air for up to 9 hours, compared to the standard 4 hours.
Q: Can E7018 electrodes be used with an AC welding machine?
Yes, E7018 electrodes are dual-purpose and can be used with both AC (Alternating Current) and DC (Direct Current) power sources.
Q: Which positions can be welded using E7018?
E7018 is an all-position electrode, suitable for PA (flat), PB (horizontal-vertical), PC (vertical-up), PD (overhead), PE, and PF positions.
Q: What is the benefit of iron powder in the coating?
Iron powder increases the amount of filler metal deposited per unit of time, significantly improving deposition efficiency and increasing productivity.
Q: Can I use unbaked E7018 for mild steel?
While mild steel can be welded with unbaked electrodes, the weld strength may not reach the maximum required specification. For high-strength or low-alloy steels, baking is mandatory.
Ready to upgrade your welding precision with E7018 electrodes?
Contact UsNeed a quick quotation for E7018? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full E7018 low hydrogen electrodes range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.