Image not available
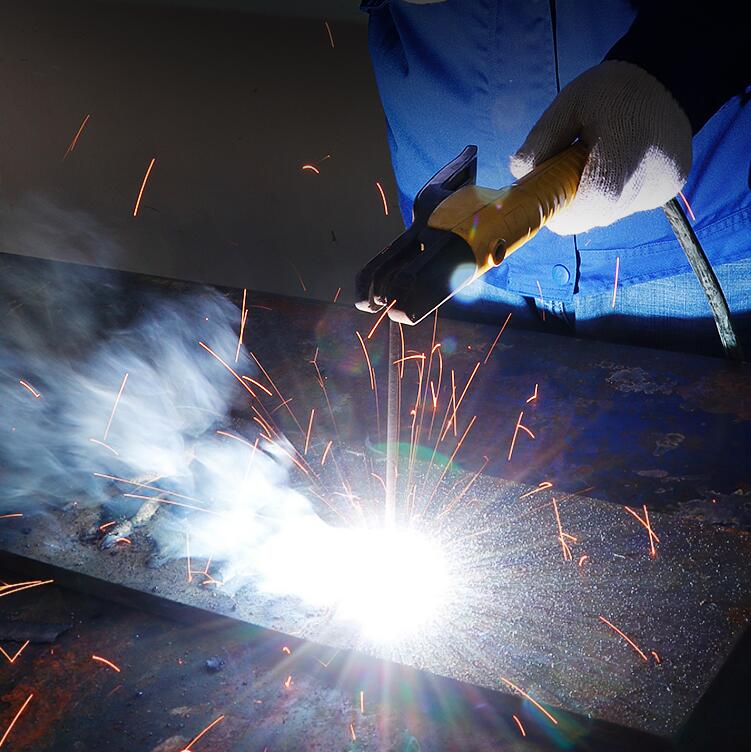
Industrial manufacturing
E6010 Cellulose Welding Rods China Factory | Leading AWS E6010 Suppliers
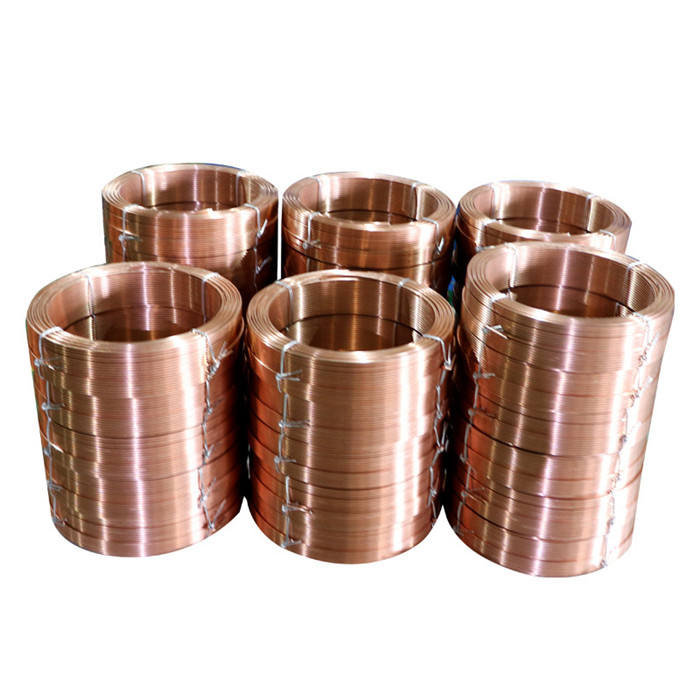
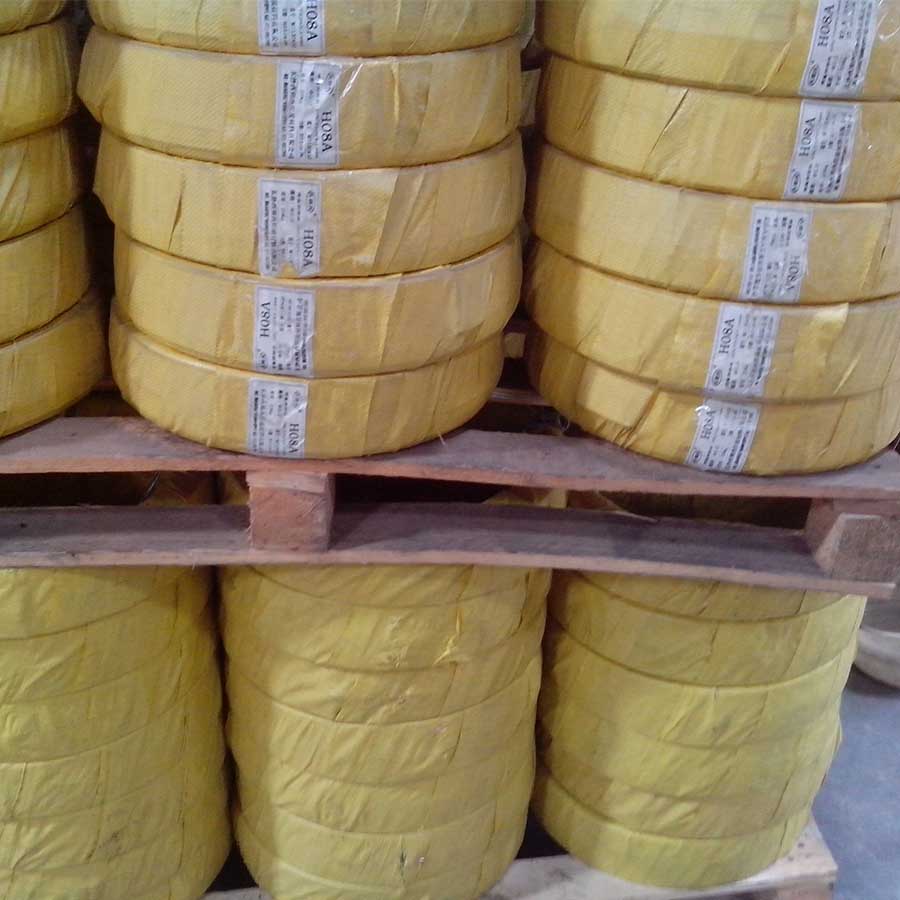
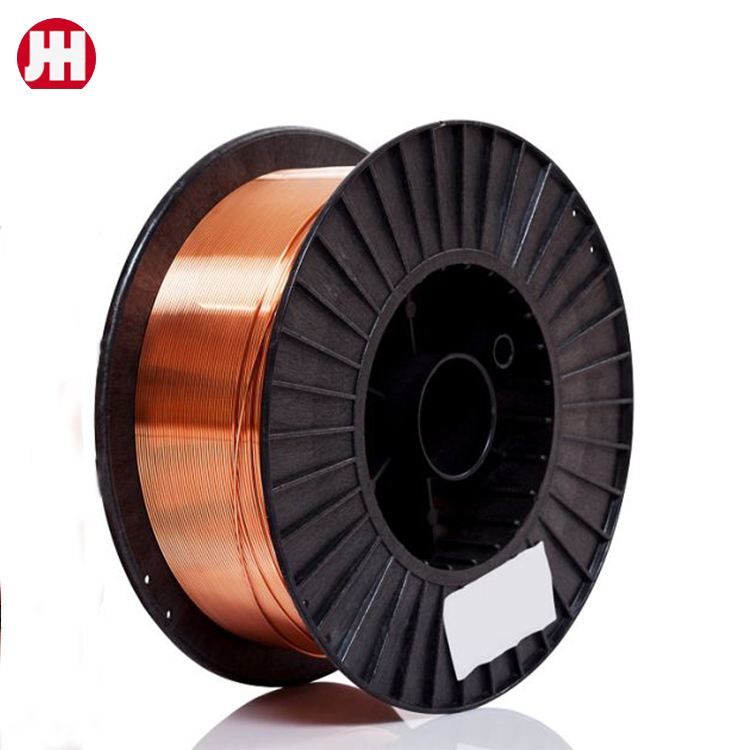
Looking for high-quality E6010 cellulose sodium type vertical downward electrodes? As a premier China factory and trusted suppliers, we provide AWS E6010 rods for efficient carbon steel pipe welding.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
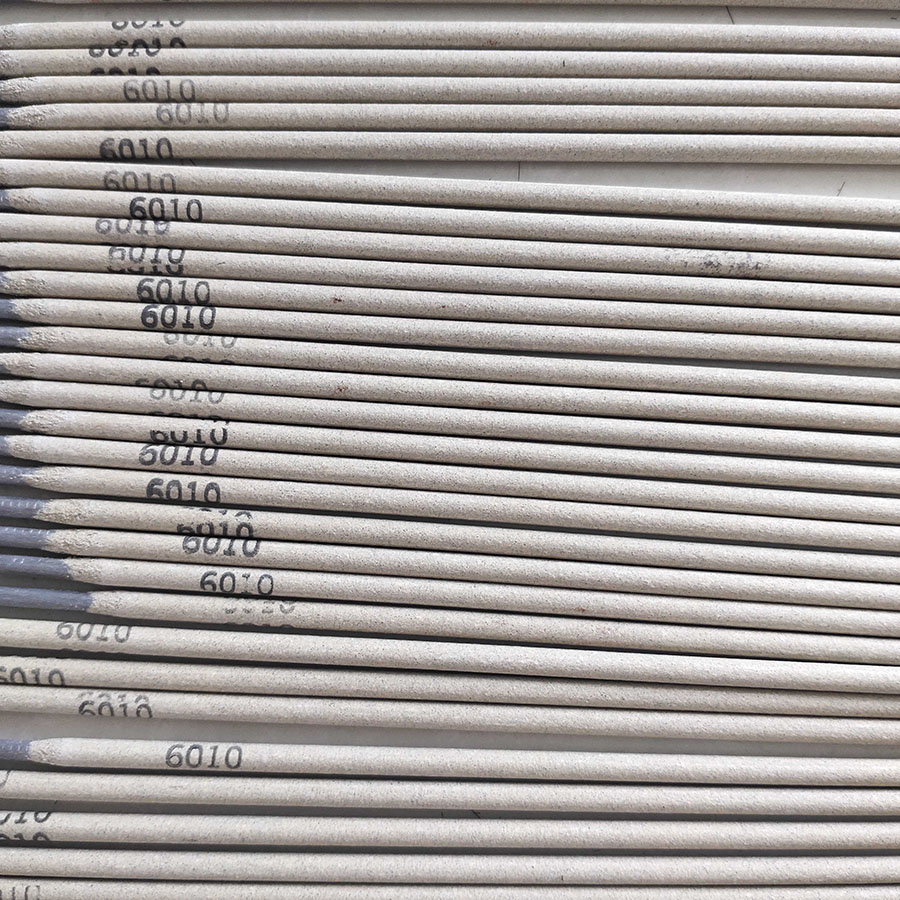
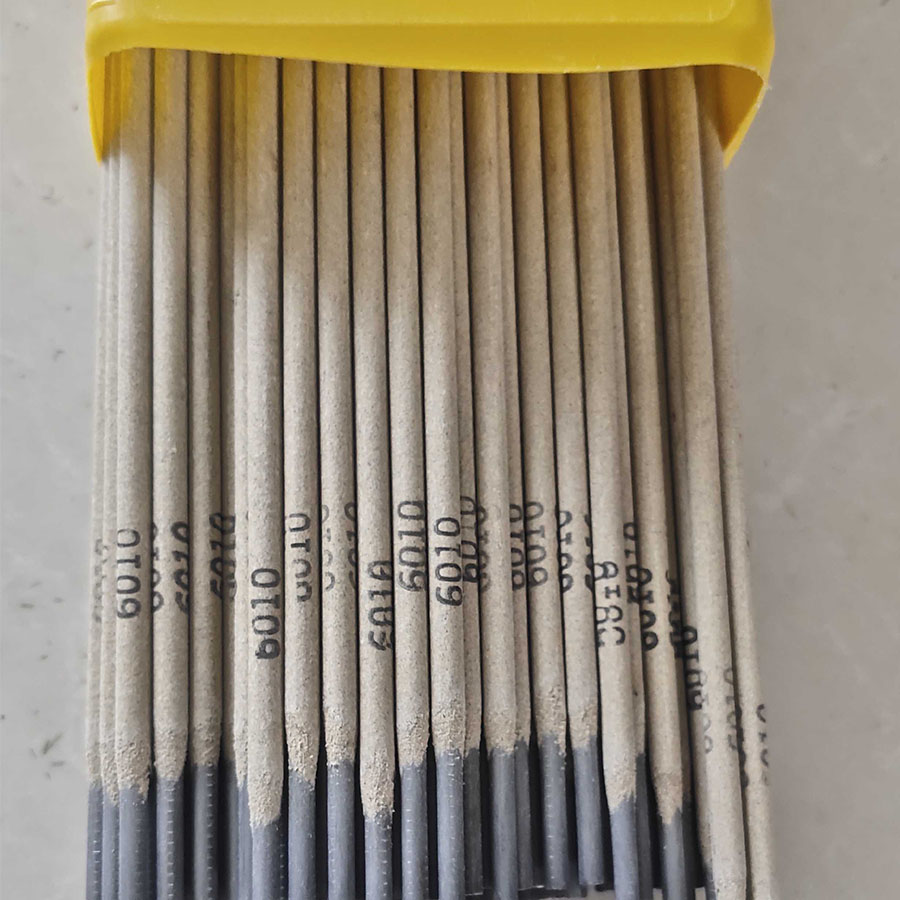
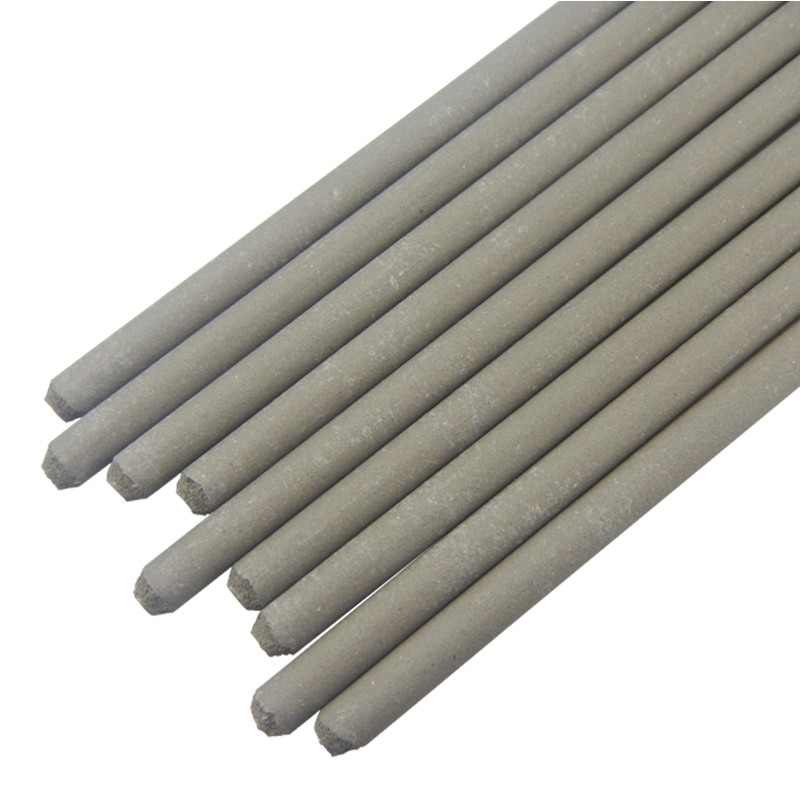
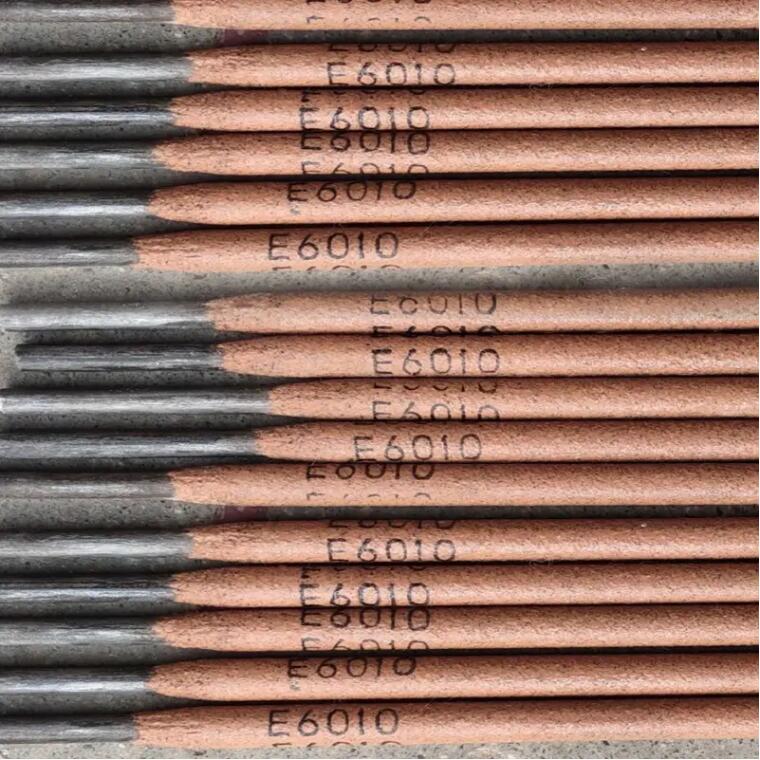
The E6010 Cellulose Welding Rod is a professional-grade, high-cellulose sodium type covered electrode specifically engineered for vertical downward welding. As a premier manufacturer in China, we provide this specialized tool to ensure high-efficiency pipe welding, offering a powerful arc blowing force that enables seamless single-sided welding with double-sided forming.
Designed for rigorous industrial applications, the E6010 electrode conforms to GB E4310 and AWS E6010 standards. It is the ideal choice for carbon steel pipe girth welding, pressure vessels, and large-scale bridge structures, delivering exceptional mechanical properties, fast deposition rates, and superior resistance to porosity and cracking.
Detailed Parameters
| Model/Grade | AWS E6010 / GB E4310 | Electrode Type | High Cellulose Sodium |
|---|---|---|---|
| Material | Alloy Steel | Welding Position | All-Position (Vertical Down) |
| Polarity | DC Reverse Polarity | Application | Carbon Steel Pipes |
| Executive Std. | GB/T5117-1995 / AWS A5.1 | Main Feature | Single-side Weld, Double-side Form |
| Storage Requirement | Closed Container / Dry Environment | Interlayer Temp. | Maximum 150°C |
Key Advantages
Anti-Crack & Porosity
Engineered for excellent crack resistance and anti-porosity, ensuring high-integrity joints in critical pipelines.
High Welding Speed
Fast deposition rates and efficient arc force significantly reduce project timelines and labor costs.
Superior Penetration
Strong arc blowing force allows for effective root pass welding with double-sided forming from one side.
Beautiful Wave Formation
Produces aesthetically pleasing welding beads with minimal slag that is exceptionally easy to remove.
All-Position Versatility
Specifically optimized for circular seam butt joints and vertical downward welding in all structural positions.
Strict Compliance
Fully conforms to international AWS A5.1 and national GB standards for guaranteed quality and safety.
Product Gallery
Management Platforms
Quality Inspection
Strict adherence to AWS and GB standards with comprehensive quality inspection forms provided.
Technical Support
Expert guidance on DC reverse polarity settings and vertical downward welding techniques.
Storage Control
Controlled environment storage to prevent humidity exposure and maintain electrode integrity.
Safety Protocols
Comprehensive safety guidelines for welders to prevent spatter burns and fire accidents.
Supply Chain
Large-scale manufacturing capacity ensuring stable lead times for global pipeline projects.
Process Optimization
Optimized for circular seam butt joints in carbon steel pipes for maximum industrial efficiency.
Investment Return Comparison
| Performance Metric | Standard Electrodes | AWS E6010 (Our Product) |
|---|---|---|
| Welding Speed | Moderate | High Velocity |
| Root Pass Effort | Double-Sided Required | Single-Sided Forming |
| Slag Removal | Time-Consuming | Easy & Fast |
| Defect Rate | Standard | Ultra-Low (Anti-Porosity) |
| Project ROI | Baseline | Significantly Increased |
Frequently Asked Questions
Q: Can E6010 welding rods be re-baked before use?
No, it is strictly forbidden to re-bake E6010 electrodes before use as it can damage the cellulose coating and affect welding performance.
Q: What is the best polarity for E6010 welding?
The E6010 welding electrode is designed to be used with DC reverse polarity (DCEP) to achieve optimal penetration and arc stability.
Q: How should E6010 electrodes be stored?
They should be stored in a closed, airtight container and used as soon as possible after opening to avoid exposure to sunlight or extreme temperature changes.
Q: What are the primary applications of the E6010 welding rod?
It is widely used for pipe girth welding, circular seam butt joints of carbon steel pipes, pressure vessels, and vertical downward welding of steel structures.
Q: What is the maximum allowable interlayer temperature?
To ensure the mechanical properties of the deposited metal, the interlayer temperature should not exceed 150°C.
Q: What safety precautions are necessary when using E6010?
Welders must wear full protective gear, including work clothes, gloves, and foot covers. Avoid rolled-up sleeves to prevent burns from welding spatter.
Looking for Premium Carbon Steel Welding Solutions?
Contact UsNeed a quick quotation for E6010? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full E6010 cellulose welding rods range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.