Image not available
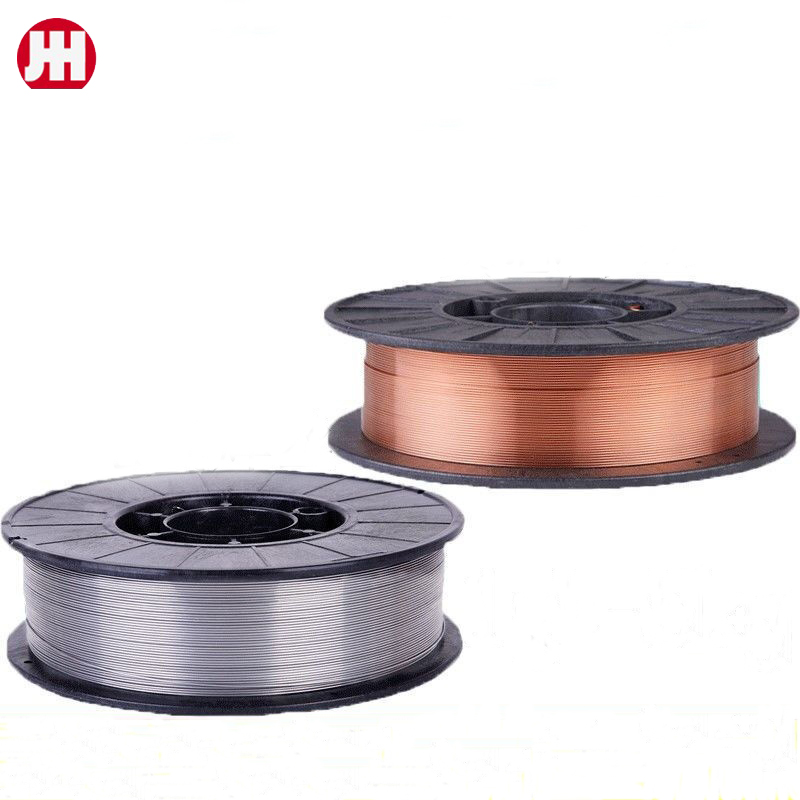
Industrial manufacturing
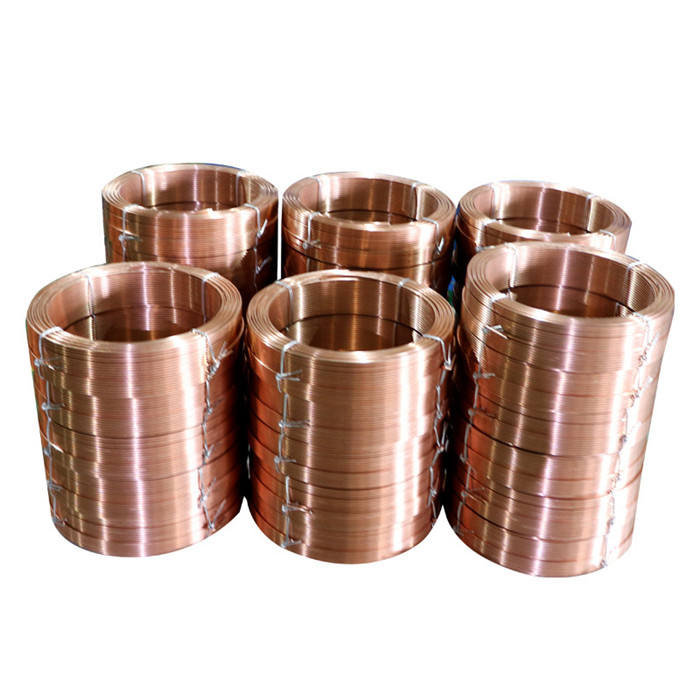
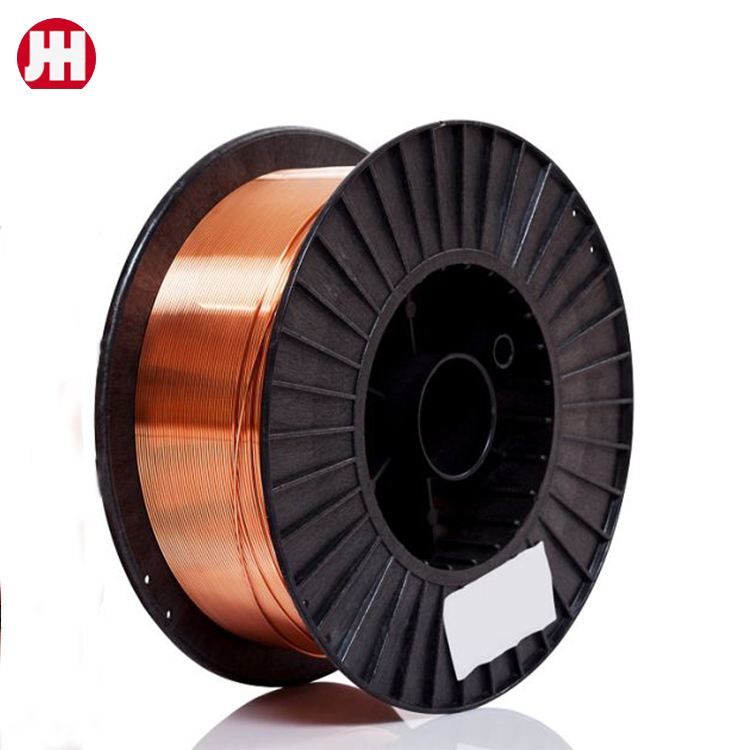
E71T-1C Gas Shield Flux Coated Welding Wire
GB/T10045 E501T-1 ISO 17632-A-T422PC2H10 NB/T 47018 E501T-1 AWS A5.36 E71T1-C1A2-CS1
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
GB/T10045 E501T-1
ISO 17632-A-T422PC2H10
NB/T 47018 E501T-1
AWS A5.36 E71T1-C1A2-CS1
This wire is CO2 gas shielded flux cored wire of titanium slag system,applying for all position welding,with excellent mechanical properties and process performance. When welding is small, the arc is stable and soft.effortless slag removal, the weld molding is beautiful. The wire approved by the classification society of ten country ,which is CCS, ABS, BV, DnV, LR, GL, NK, KR, CWB, RINA . Approval grade is 3YH10.
1.Direct Current Electrode Positive(DCEP)welding.(Welding wire connecting anode)
2, Use CO2 as shielded gas ,whose purity is more than 99.9%, and flow rate is 20-25L/min.
3, when in multi pass welding, keep the layer temperature at about 150 to 200 degrees celsius.
4, In order to prevent the occurrence of pores,
please the remove the grease and rust from the surface of base metal before welding.
5, the preservation of welding wire: wire has been taken measures to resist
moisture before using.It should be used as soon as possible when opening
the package , do not leave the welding wire has not been used up
for a long time in the air.
6,Due to the softer solid wire ,do not lock the pressure roller of wire feeding device too tight.
Need a quick quotation for E71T-1C? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full flux cored welding wire range.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.