Image not available
Industrial manufacturing
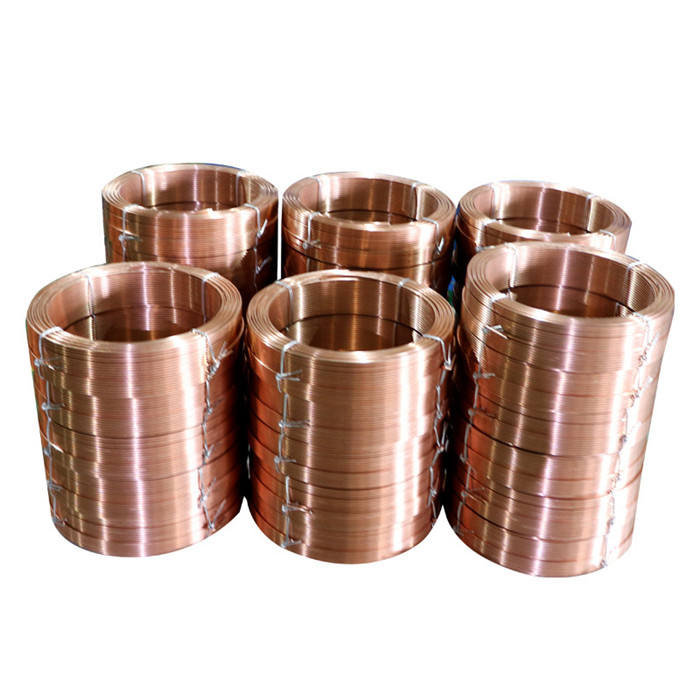
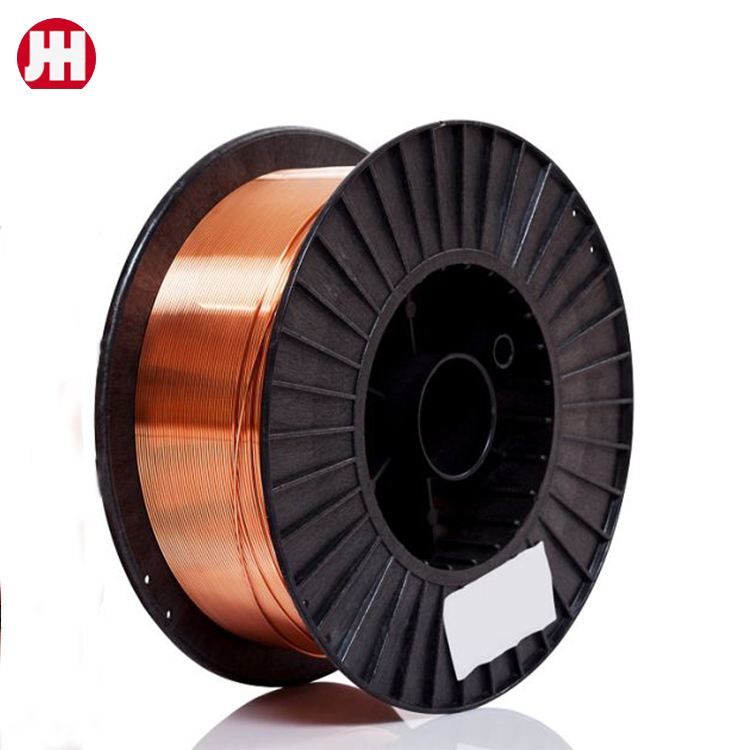
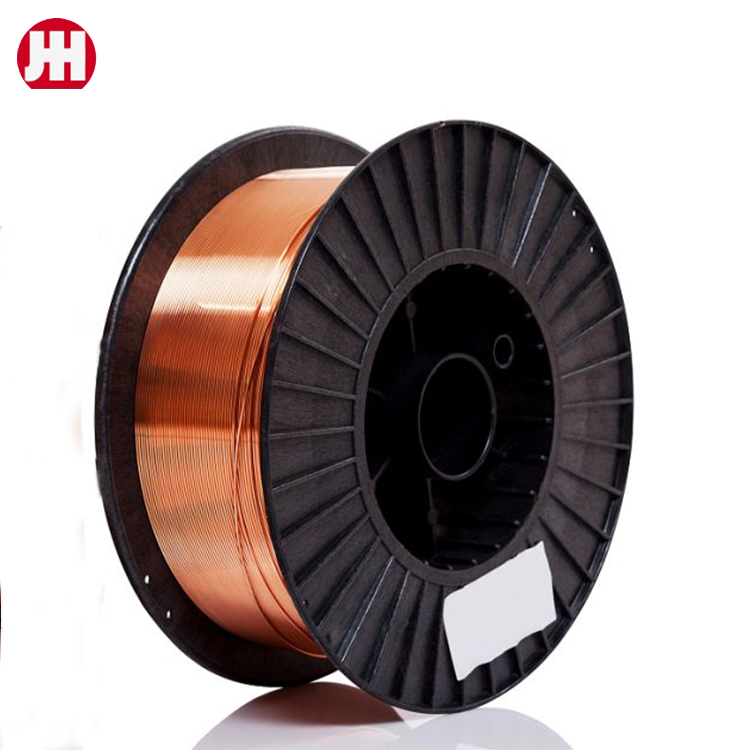
Co2 Solid Welding Wire Solder Wire
The Welding Wire ER70S-6 is 500MPa level carbon steel wire. It take CO2 or 80%Ar + 20%CO2 gas shielded arc welding. The welding spatter is small, and it has beautiful appearance, high cladding efficiency and small weld metal porosity sensibility. The welding technology of all positions is good.
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
Alambre wire
The Welding Wire ER70S-6 is 500MPa level carbon steel wire. It take CO2 or 80%Ar + 20%CO2 gas shielded arc welding. The welding
spatter is small, and it has beautiful appearance, high cladding efficiency and small weld metal porosity sensibility. The welding
technology of all positions is good.
Welding Positions:
PA、PB、PC、PD、PE、PF
Gas shielded welding is divided into inert gas shielded welding (TIG welding and MIG welding), active gas shielded welding (MAG welding) and self shielded welding. Pure Ar is used for TIG welding, and Ar + 2% O2 or Ar + 5% CO2 is generally used for MIG welding. MAG welding mainly uses CO2 gas. In order to improve the process performance of CO2 welding, CO2+Ar or CO2+Ar+O2 mixed gas or flux cored wire can also be used.
- TIG welding wire
TIG welding sometimes does not add filler wire, which is directly connected after being heated and melted by the base metal to be welded, and sometimes adds filler wire, because the shielding gas is pure Ar, non-oxidizing, and the composition of the wire does not change basically after melting, so the composition of the wire is the welding wire seam components. Some also use the base metal composition as the welding wire composition to make the weld composition consistent with the base metal. During TIG welding, the welding energy is small, the weld strength, plasticity and toughness are good, and it is easy to meet the performance requirements.
- MIG and MAG welding wire
The MIG method is mainly used for welding high-alloy steels such as stainless steel. In order to improve the arc characteristics, add an appropriate amount of 02 or CO2 gas to the Ar gas, which becomes the MAG method. When welding alloy steel, the use of Ar + 5% CO2 can improve the anti-porosity ability of the weld. However, when welding ultra-low carbon stainless steel, Ar + 5% CO2 mixed gas cannot be used, and only Ar + 2% O2 mixed gas can be used to prevent weld carburization. At present, MIG welding of low alloy steel is gradually being replaced by MAG welding of Ar + 20% CO2. During MAG welding, due to the oxidizing properties of the shielding gas, the content of deoxidizing elements such as Si and Mn in the welding wire should be appropriately increased. Other components can be the same as the base metal, or they can be different. When welding high-strength steel, the content of C in the weld is usually lower than that of the base metal, and the content of Mn should be higher than that of the base metal. This is not only for deoxidation, but also a requirement for the alloy composition of the weld. In order to improve the low temperature toughness, the content of Si in the weld should not be too high.
Need a quick quotation for welding wire? Chat with us on WhatsApp or email info@steeltoolschina.com.
Browse the copper coated welding wire collection.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.