Image not available
Industrial manufacturing
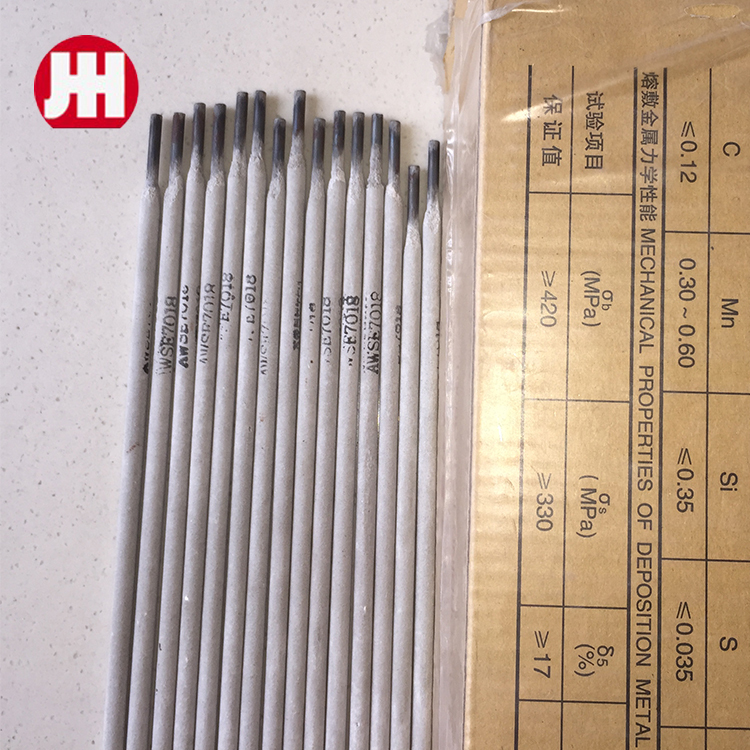
Welding Rod Eletrodo AWS E7018
E7018 is a multi-purpose electrode with excellent handling properties. 7018 performs especially well when welding mild steel or low alloy steel, such as bridges, construction,
SupplierHEBEI YUJINHONG TECHNOLOGY CO.,LTD.www.steeltoolschina.com
Source categories
About this product
Product information from the supplier.
E7018 is a multi-purpose electrode with excellent handling properties. 7018 performs especially well when welding mild steel or low alloy steel, such as bridges, construction, shipbuilding and pressure vessel manufacturing, etc. The E7018 can also be used in construction and maintenance of a range of engineering machinery such as bulldozers, agricultural or mining equipment.
AWS E7018 Carbon Steel Electrode Carbon Steel Electrode Description: E7018 is a carbon steel electrode with iron powder and low hydrogen potassium coating. Both AC and DC can be used for all-position welding. Its characteristic is that the coating contains iron powder, which can reduce the number of welding layers. Uses: Suitable for welding carbon steel and low alloy steel, such as 16Mn, etc.
Relevant standards GB/T 5117: E5018 AWS A5.1: E7018 ASME SFA-5.1
User guides
Bake the electrode at 300°C for 60 minutes before use. If the electrode is exposed to the air for a long time, it is recommended to bake at 300-350°C for 60-120 minutes. Welding rods that have been opened should be stored at 100-150°C.
Remove water, dirt, oil, etc. from the metal surface of the base metal before welding to prevent cracks and pores.
The back-and-forward method should be used to prevent air holes or pits at the arc strike.
The arc length should be kept as short as possible during welding. If swinging is required, the swinging range should not exceed 3 times the diameter of the electrode.
E7018 electrode is an alkaline, perovskite type electrode, which belongs to low water hydrogen, low carbon steel electrode. Its electroslag ability is strong, the droplet is easy to be stable and less sputtering, it is suitable for welding various strength grades of low carbon steel and low alloy steel structures, such as straight seams, transverse seams, corner seams, etc., suitable for filling, Back welding, stable tetrahedral arc opening, and strong power supply faults. It is particularly excellent in preventing noise and reducing the risk of explosion. At the same time, it also has the advantages of high output, power saving, and low waste rate. Generally speaking, the E7018 electrode performs better when welding workpieces that require high strength. It has the advantages of almost no spattering in the deposition and good formability, and brings higher comfort and safety to workers during the welding process.
Need a quick quotation for E7018? Chat with us on WhatsApp or email info@steeltoolschina.com.
See the full E7018 low hydrogen electrodes range, or browse all welding electrodes.
More from this supplier
HEBEI YUJINHONG TECHNOLOGY CO.,LTD.