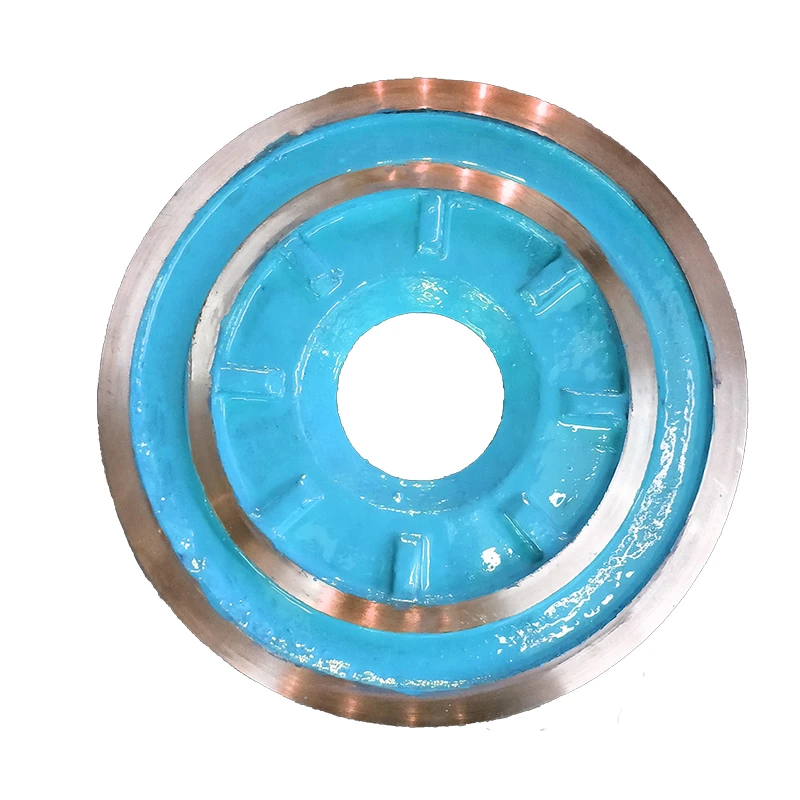
Image not available
Industrial manufacturing
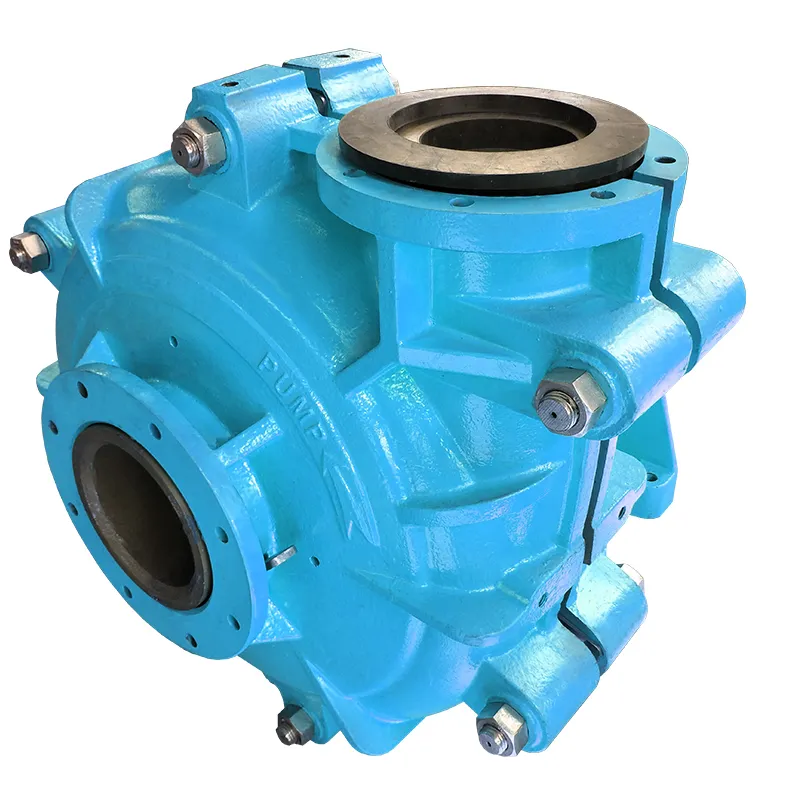
MineMaxx 86EAH Horizontal Slurry Pump China Factory and Leading Suppliers
Looking for reliable China suppliers? Our MineMaxx 86E-AH slurry pump is a high-performance solution from a leading factory designed for abrasive and corrosive slurries in mining and power generation.
SupplierHEBEI MINEMAXX TECHNOLOGY CO.,LTD.www.minemaxx.com
Source categories
About this product
Product information from the supplier.
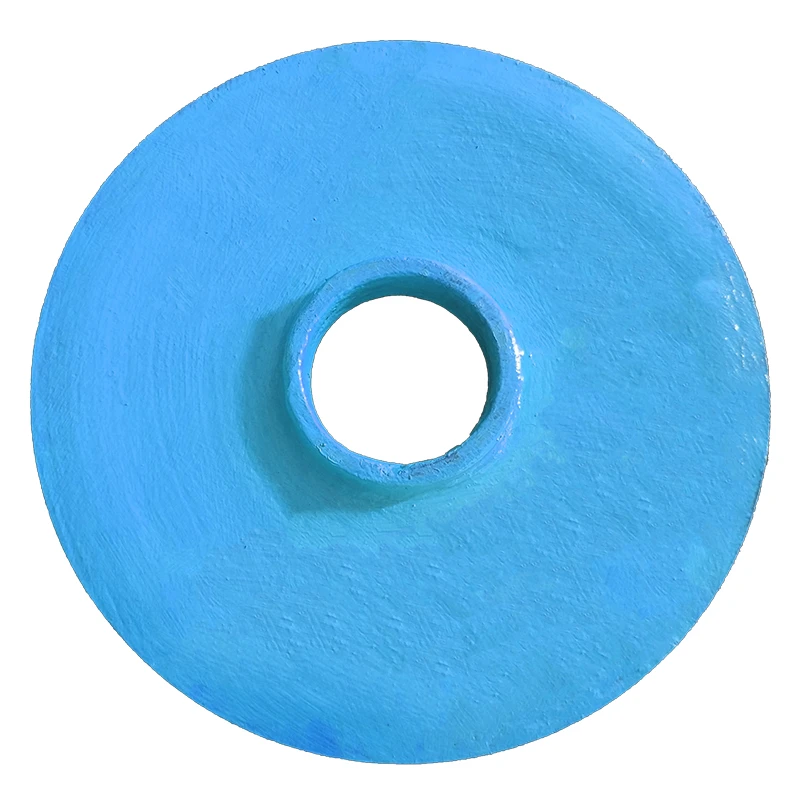
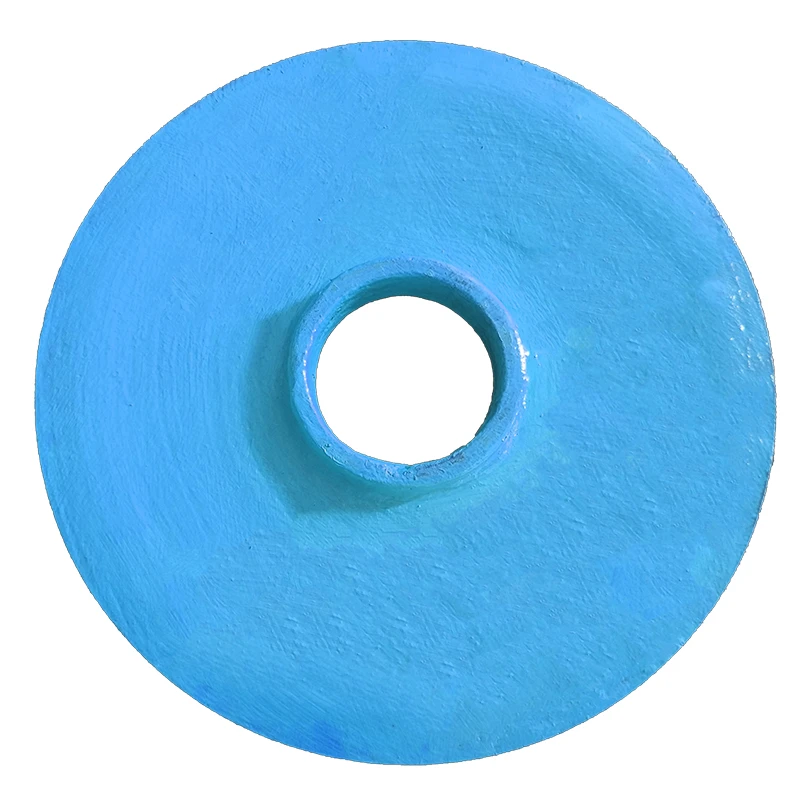
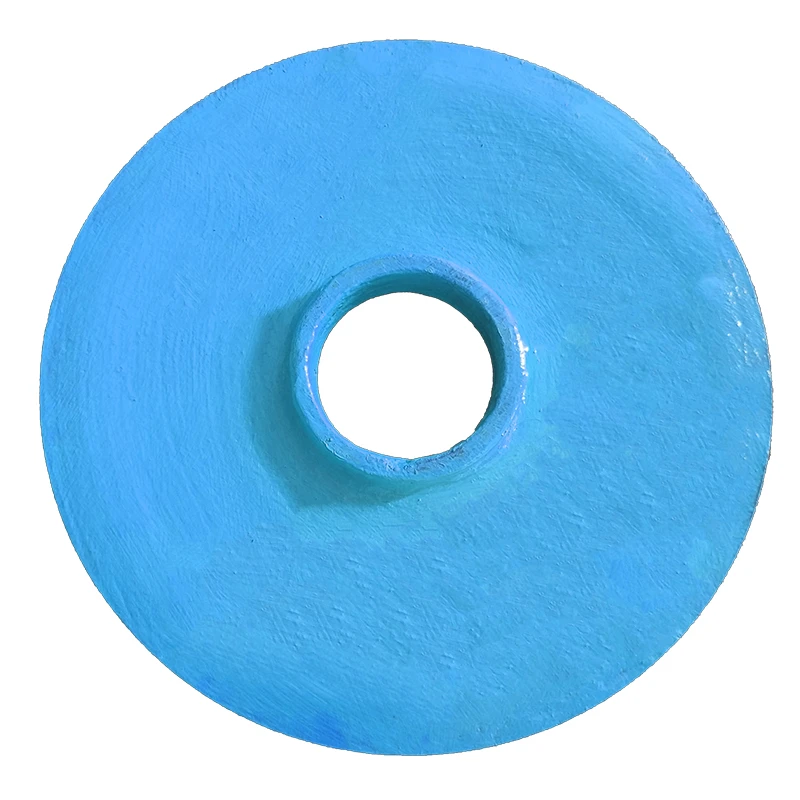
The MineMaxx 8/6E-AH Horizontal Slurry Pump is a high-performance industrial powerhouse engineered specifically for the most demanding abrasive and corrosive environments. Designed for heavy-duty slurry handling, this robust pump integrates advanced hydraulic engineering with premium materials to ensure maximum uptime and operational efficiency in mining and mineral processing sectors.
Equipped with a high-efficiency impeller and a large diameter shaft, the 8/6E-AH model excels in transporting high-density slurries and large particles. Whether applied to mill discharge or tailings transfer, its superior construction minimizes wear and optimizes flow, providing a dependable solution for industries where reliability is non-negotiable.
Detailed Parameters
| Model | 8/6E-AH | Max Motor Power | 120 Kw |
|---|---|---|---|
| Capacity (m³/h) | 360-828 | Head H (m) | 10-61 |
| Pump Speed (r/min) | 400-1140 | Efficiency (%) | 65-72 |
| NPSH (m) | 2-10 | Liner/Impeller Material | M / RU |
| Metal Weight (KG) | 1424 | Rubber Weight (KG) | 944 |
Key Advantages
Robust Construction
Heavy-duty casing and thick-walled impellers engineered to withstand extreme abrasion from slurry.
Extended Service Life
Unique double-casing design provides superior protection against wear and reduces maintenance frequency.
High Particle Handling
Large diameter shaft and efficient impeller allow for seamless transport of high-density slurries.
Versatile Sealing
Multiple sealing options available to ensure leak-proof operation across diverse industrial conditions.
High Flow Efficiency
Optimized hydraulics achieving flow rates up to 828 m³/h for maximum throughput.
Industrial Versatility
Ideal for tailings, sand, gravel, and chemical waste streams in mining and power generation.
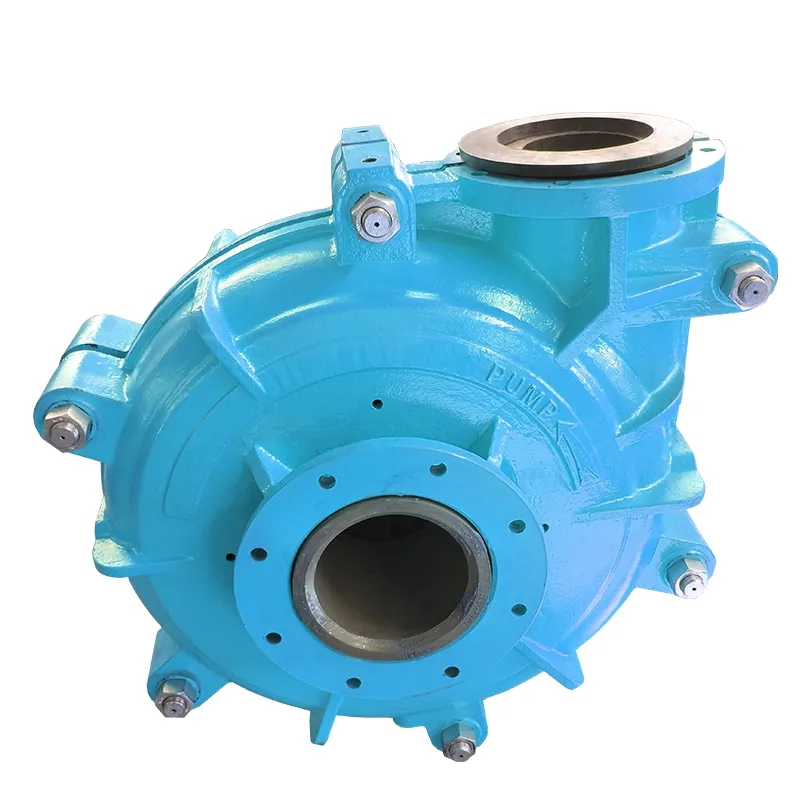
Product Gallery
Management Platforms
Wear Parts Inventory
Efficient tracking of Impellers, Throat Bushes, and Liner plates to prevent downtime.
Maintenance Scheduling
Systematic monitoring of pump speed and efficiency for predictive maintenance.
Performance Alerts
Real-time notifications regarding NPSH levels and motor power fluctuations.
Wear Monitoring
Advanced tracking of casing thickness to optimize replacement cycles.
Spare Parts Logistics
Streamlined procurement for Bearing Assemblies and Frame Plate Liners.
Hydraulic Optimization
Adjustment of pump speed (r/min) to match slurry density and flow requirements.
Investment Return Comparison
| Metric | Standard Pump | MineMaxx 8/6E-AH |
|---|---|---|
| Service Life | Short (High Wear) | Long (Double-Casing) |
| Maintenance Cycle | Frequent | Extended |
| Energy Efficiency | Moderate | Optimized (up to 72%) |
| Handling Capacity | Limited Solids | High-Density Slurries |
| Total Cost of Ownership | High (Parts Replace) | Low (Durability Focus) |
Frequently Asked Questions
Q: What materials are used for the 8/6E-AH pump liners and impellers?
The pump utilizes high-grade M (Metal) and RU (Rubber) materials, depending on the specific abrasiveness and corrosiveness of the slurry being handled.
Q: Which industries are best suited for the MineMaxx Horizontal Slurry Pump?
It is ideal for mining, mineral processing, coal preparation, power generation, and chemical processing, specifically for handling tailings and industrial waste.
Q: How does the double-casing design benefit the pump's operation?
The double-casing provides an additional layer of protection against the abrasive nature of slurries, significantly extending the pump's operational lifespan.
Q: What is the maximum flow rate the 8/6E-AH can achieve?
The MineMaxx 8/6E-AH can handle a maximum flow rate of up to 828 cubic meters per hour.
Q: Can this pump handle large particles in the slurry?
Yes, thanks to its high-efficiency impeller and large diameter shaft, it is specifically designed to handle large particles and high-density slurries.
Q: What are the common applications for this specific model?
Common applications include mill discharge, cyclone feed, and tailings transfer where reliable, heavy-duty slurry handling is essential.
Ready to Optimize Your Slurry Handling Process?
Contact UsMore from this supplier
HEBEI MINEMAXX TECHNOLOGY CO.,LTD.