Image not available
Industrial manufacturing
Industrial Coalfired Hot Water Boilers Factory and Suppliers in China
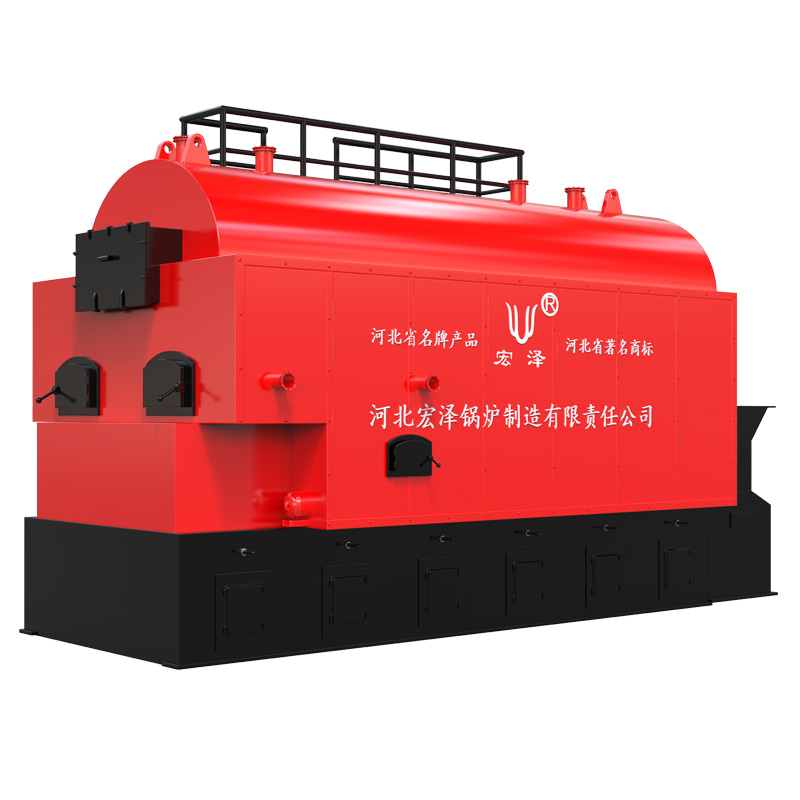
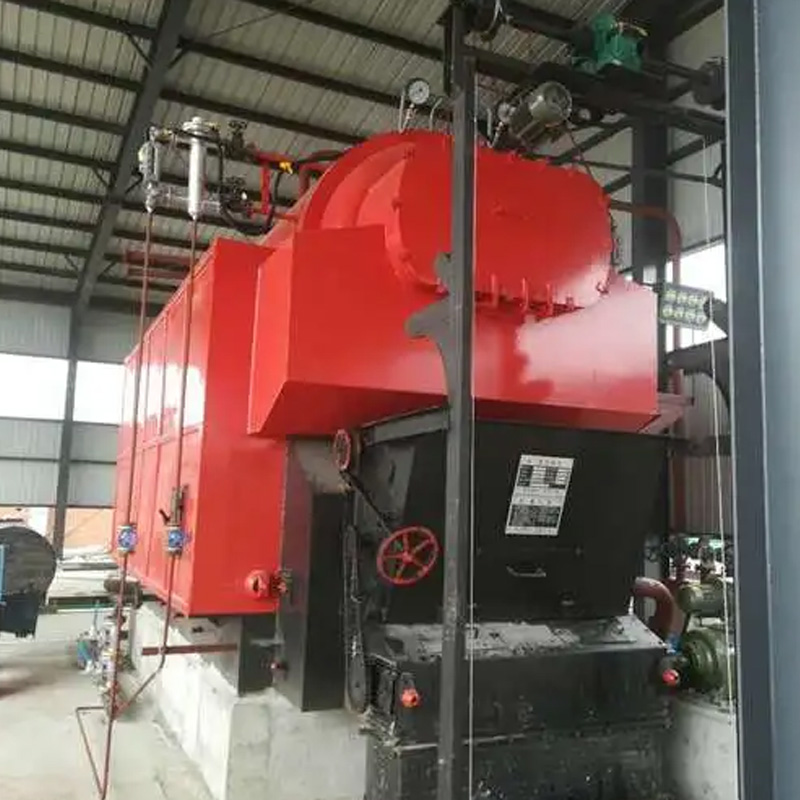
Leading China factory and suppliers of high-performance coal-fired hot water boilers. Featuring thermal power from 0.7-140 MW and pressure 0.7-2.5 MPa. Our boilers utilize advanced water-cooled walls and flue pipes to convert lignite, anthracite, and bituminous coal into efficient circulating hot water for industrial heating.
SupplierHEBEI HONGZE BOILER MANUFACTURING CO., LTD.www.hzsteamboiler.com
Source categories
About this product
Product information from the supplier.
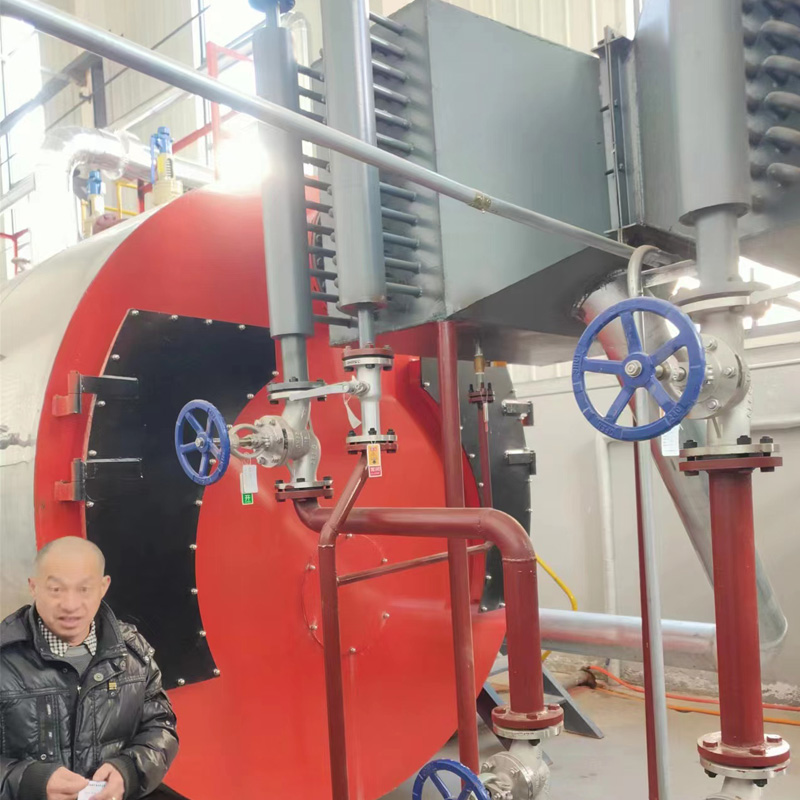
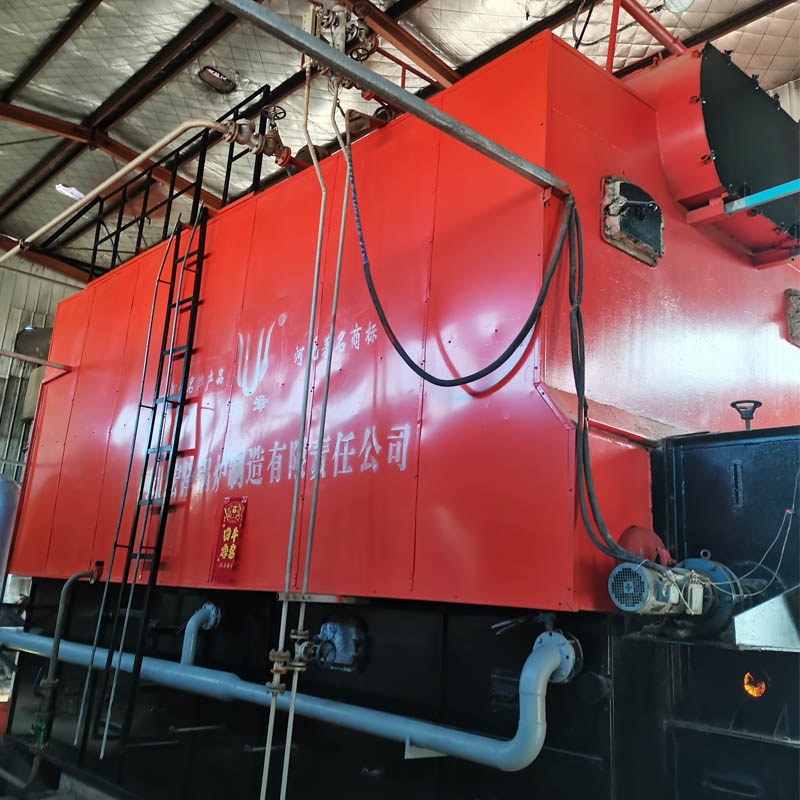
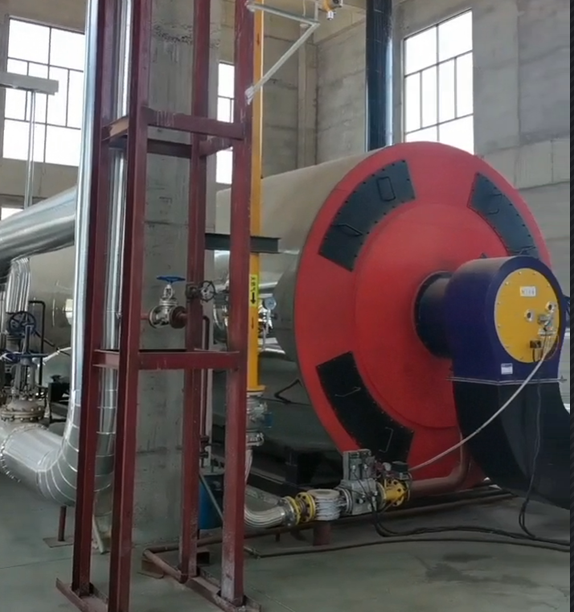
Our high-performance Coal-fired Hot Water Boilers are engineered for maximum thermal efficiency and long-term industrial reliability. Utilizing a sophisticated three-way water-fired tube structure with a longitudinal arrangement, these boilers are designed to meet the rigorous heating demands of various industrial sectors while maintaining a compact footprint.
The furnace chamber is densely integrated with water-cooled wall tubes, optimizing the heat exchange surface and extending the flue gas flow path. This strategic design significantly lowers exhaust temperatures and boosts overall thermal efficiency, resulting in reduced operational costs and a more sustainable energy profile for your facility.
Detailed Parameters
| Thermal Power Range | 0.7 MW to 63 MW | Working Pressure | 0.7 MPa to 1.25 MPa |
|---|---|---|---|
| Output Water Temp | 95℃ to 130℃ | Feeding Water Temp | 70℃ (Standard) |
| Max Thermal Efficiency | Up to 88.9% | Exhaust Gas Temp | 134.1℃ to 168.6℃ |
| Structure Type | Horizontal Water-fired Tube | Wall Design | Water-cooled Wall Tubes |
| Model Series | DZL Series (AII) | Design Focus | Low Exhaust Temperature |
Key Advantages
Robust Architecture
Featuring a longitudinal three-way water-fired tube structure for enhanced structural integrity and durability.
High Thermal Efficiency
Achieves up to 88.9% efficiency through optimized heat transfer and reduced energy waste.
Optimized Heat Transfer
Densely covered water-cooled wall tubes maximize the heating area for faster water temperature rise.
Low Exhaust Temp
Extended flue gas flow paths ensure lower exhaust temperatures, preventing heat loss.
Compact Layout
A reasonable and compact design allows for easier installation and space utilization in factories.
Economical Operation
Reduced fuel consumption and lower operating costs make it a highly economical choice for enterprises.
Product Gallery
Management Platforms
Fuel Management
Optimized coal feeding systems to ensure steady combustion and minimal waste.
Pressure Control
Precision pressure monitoring to maintain stability across all thermal power levels.
Safety Monitoring
Integrated alarm systems for real-time tracking of water levels and exhaust temperatures.
Thermal Tracking
Dynamic monitoring of thermal efficiency to ensure peak performance during operation.
Water Cycle Management
Advanced feeding water temperature control to maximize the heating cycle.
Maintenance Scheduling
Scheduled cleaning of water-cooled walls to prevent scale and maintain heat transfer.
Investment Return Comparison
| Feature | Standard Boilers | Our Coal-fired Boiler |
|---|---|---|
| Thermal Efficiency | 75% - 82% | Up to 88.9% |
| Operational Cost | Higher Fuel Waste | Optimized Fuel Usage |
| Exhaust Temp | High Heat Loss | Precisely Controlled/Low |
| Heat Exchange Area | Conventional | Enhanced (Water-cooled Walls) |
| ROI Period | Longer | Faster due to Energy Savings |
Frequently Asked Questions
Q: What are the main advantages of the water-cooled wall tube design?
The water-cooled wall tubes increase the heating surface area, allowing for better heat absorption from the flue gas, which significantly boosts overall thermal efficiency and reduces exhaust temperatures.
Q: How does the three-way water-fired tube structure improve performance?
This structure optimizes the flow of water and flue gas, ensuring a more uniform heat distribution and a longer flow path, which is critical for achieving high thermal efficiency in coal-fired boilers.
Q: What is the maximum thermal power available for this series?
The DZL series offers a wide range of capacities, reaching a maximum rated thermal power of 63 MW to accommodate large-scale industrial heating needs.
Q: Can these boilers handle different rated working pressures?
Yes, depending on the model, our boilers support rated working pressures ranging from 0.7 MPa up to 1.25 MPa to suit various application requirements.
Q: How does this boiler help in reducing operation costs?
By maximizing thermal efficiency (up to 88.9%) and lowering exhaust gas temperatures, the boiler consumes less fuel to produce the same amount of heat, leading to significant long-term cost savings.
Q: What is the typical output water temperature for these models?
Depending on the selected model, the rated output water temperature ranges from 95℃ to 130℃, providing flexibility for different industrial heating processes.
Ready to Optimize Your Industrial Heating Efficiency?
Contact UsMore from this supplier
HEBEI HONGZE BOILER MANUFACTURING CO., LTD.