Image not available
Industrial manufacturing
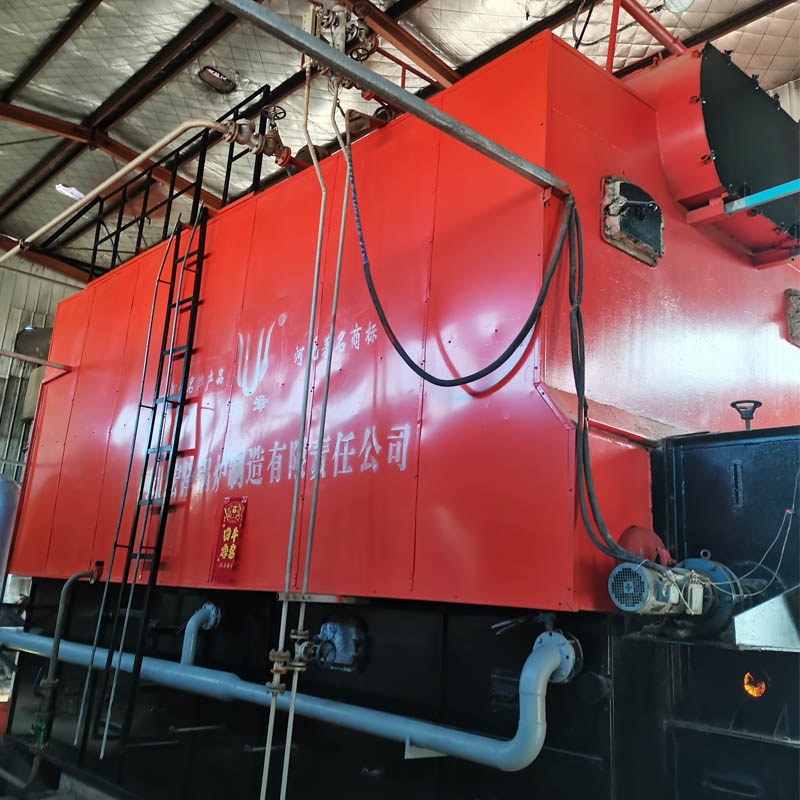
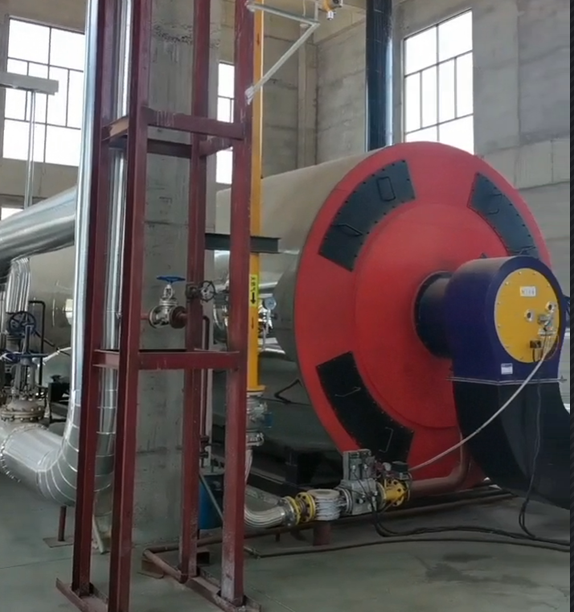
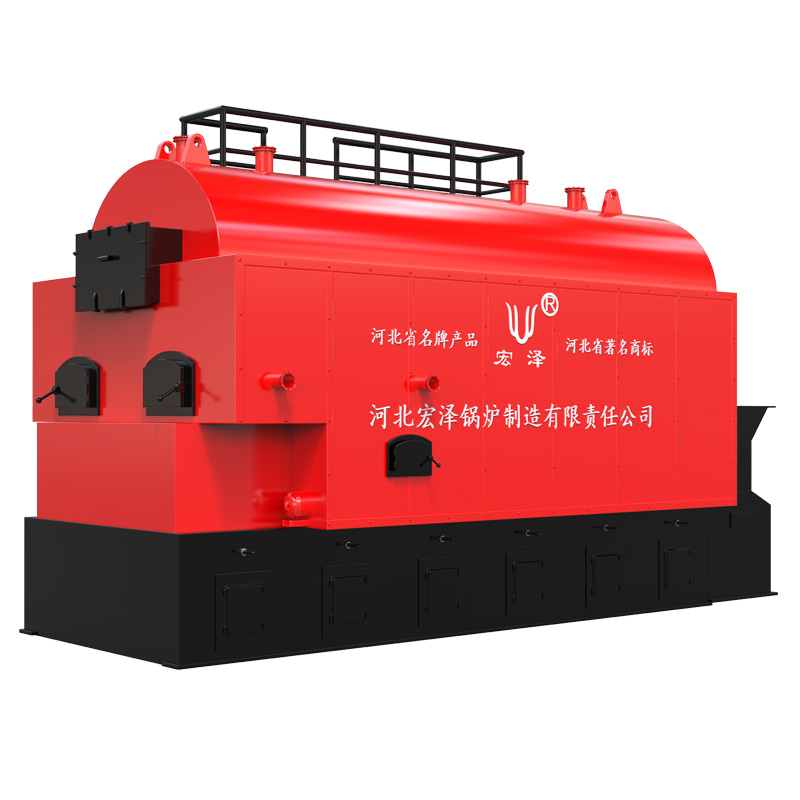
Industrial Gas and Oil Hot Water Boiler Factory Leading China Suppliers
Looking for reliable China suppliers? Our boiler factory offers high-efficiency Gas and Oil Hot Water Boilers with rated thermal power 0.7-140 MW, working pressure 0.7-1.25MP, and NOx emission ≤ 30mg. Compatible with Natural gas, Lpg, biogas, and coke oven gas.
SupplierHEBEI HONGZE BOILER MANUFACTURING CO., LTD.www.hzsteamboiler.com
Source categories
About this product
Product information from the supplier.
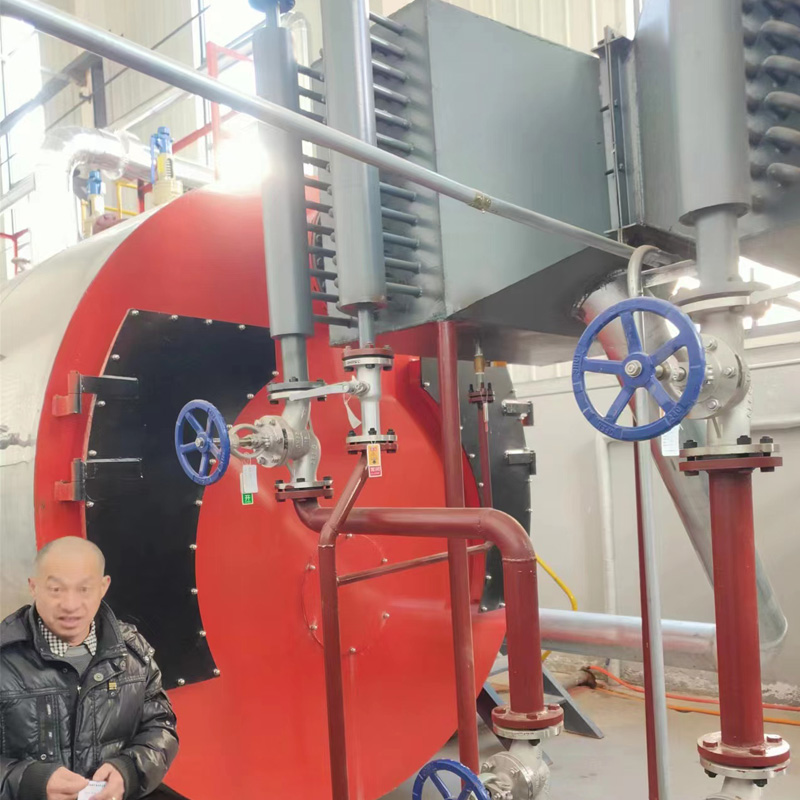
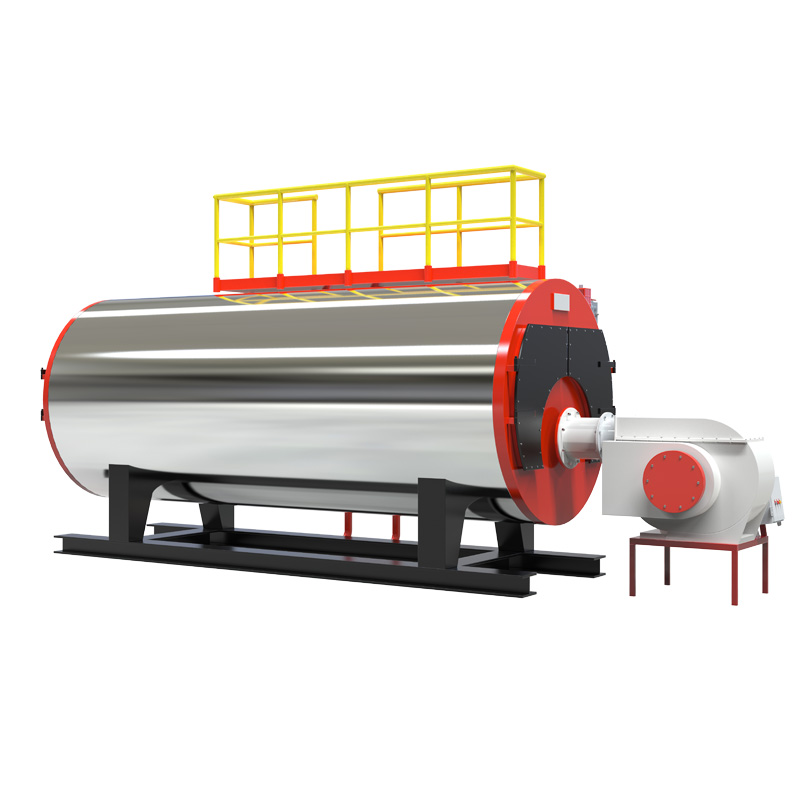
Our advanced Gas and Oil Hot Water Boilers are engineered for maximum thermal efficiency, utilizing a precision combustion process where natural gas or oil fuels heat the water within the boiler pot. By continuously optimizing the energy release from the furnace, these systems generate a stable and high-temperature hot water supply tailored for demanding industrial and commercial applications.
Designed with a focus on sustainability and safety, these boilers integrate cutting-edge technology to reduce NOx emissions and minimize heat loss. From the corrugated liner to the fully automated control systems, every component is optimized to ensure reliable operation, lower operational costs, and compliance with strict environmental standards.
Detailed Parameters
| Thermal Power Range | 0.7 MW to 46 MW | Working Pressure | 0.7 MPa to 1.25 MPa |
|---|---|---|---|
| Output Water Temp | 95℃ to 130℃ | Feeding Water Temp | 70℃ (Standard) |
| Max Thermal Efficiency | Up to 98.1% | Exhaust Gas Temp | 134℃ to 168.62℃ |
| Burner Type | Imported Low-NOx Burner | Emission Standard | NOx ≤ 30mg/Nm³ |
| Control System | Full-Automatic PLC | Safety Features | Over-temp & Over-pressure Warning |
Key Advantages
Maximum Efficiency
Large heating area of the pot barrel ensures full fuel combustion for industry-leading thermal efficiency.
Eco-Friendly Combustion
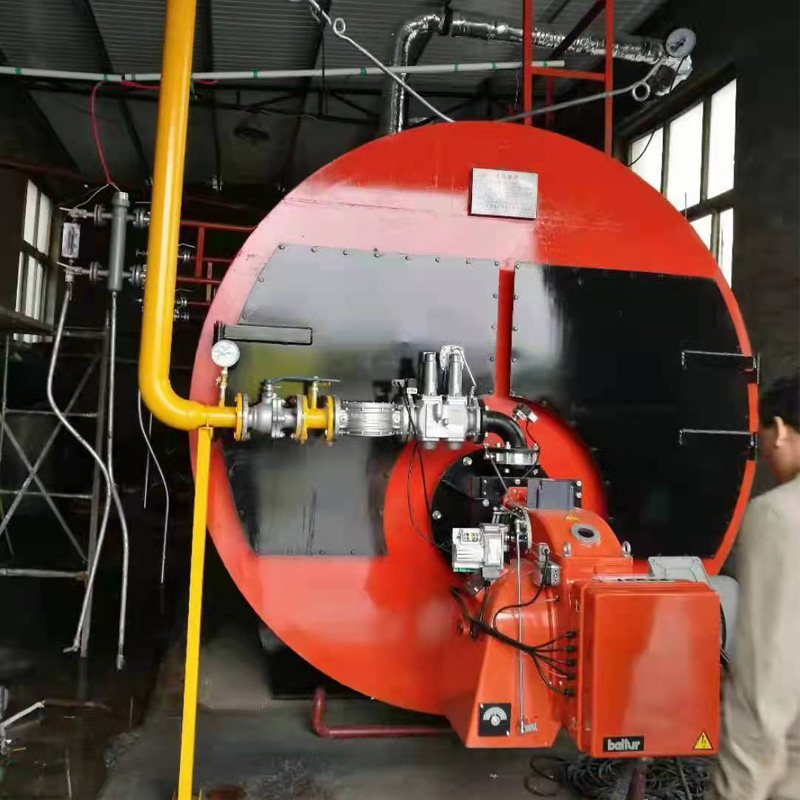
Imported burners strictly maintain NOx emissions below 30mg/Nm³, meeting global environmental norms.
Energy Saving Design
Corrugated liners, threaded flue pipes, and condensers significantly reduce waste heat loss.
Enhanced Safety
High-sensitivity gas valve groups prevent leaks and safeguard against potential industrial accidents.
Smart Automation
Fully automatic control system simplifies operation and ensures consistent water temperatures.
Easy Maintenance
Integrated safety warnings for temperature and pressure allow for proactive and simple upkeep.
Product Gallery
Management Platforms
Thermal Monitoring
Real-time tracking of water temperature and fuel consumption levels.
Pressure Regulation
Automated pressure adjustments to prevent system overload and ensure stability.
Safety Alerts
Instant notifications for over-temperature or over-pressure events.
Emission Control
Continuous monitoring of NOx and exhaust gas temperatures for compliance.
Fuel Optimization
Algorithm-based burner adjustment to minimize fuel waste.
System Diagnostics
Digital health checks for simplified maintenance and fault detection.
Investment Return Comparison
| Performance Metric | Standard Boiler | Our High-Efficiency Boiler |
|---|---|---|
| Thermal Efficiency | 85% - 90% | 93.8% - 98.1% |
| NOx Emissions | Moderate | Ultra-Low (≤30mg/Nm³) |
| Fuel Consumption | Baseline | Reduced by 10% - 15% |
| Maintenance Cost | High Frequency | Low (Auto-Diagnostics) |
| Operational Life | Standard | Extended via Corrugated Liner |
Frequently Asked Questions
Q: What is the main difference between a hot water boiler and a steam boiler?
A hot water boiler heats water to a specific temperature without boiling it, primarily used for space heating and process heating, whereas a steam boiler converts water into steam for high-energy industrial processes.
Q: How does the corrugated liner improve efficiency?
The corrugated liner increases the heat transfer surface area and creates turbulence in the flue gas, which slows down the gas flow and maximizes heat absorption into the water.
Q: Is the boiler compatible with both natural gas and oil?
Yes, our models are designed for versatility and can be configured for either natural gas or oil fuel depending on your facility's requirements.
Q: What safety measures are included to prevent gas leaks?
We utilize high-sensitivity gas valve groups and integrated electronic sensors that trigger an automatic shutdown if a leak or abnormal pressure is detected.
Q: How often should the boiler undergo maintenance?
While our automated systems simplify maintenance, we recommend a professional inspection every 6-12 months to ensure optimal thermal efficiency and safety compliance.
Q: Can the output water temperature be adjusted?
Yes, the full-automatic control system allows users to set and maintain precise output water temperatures ranging from 95℃ up to 130℃ depending on the model.
Ready to Optimize Your Industrial Heating System?
Contact UsMore from this supplier
HEBEI HONGZE BOILER MANUFACTURING CO., LTD.